Managing Intermetallic Compound Growth in High Temperature Board Assemblies
Specify nickel barrier finishes, clamp reflow thermal budgets, and reject lots where intermetallic thickness exceeds four micrometers after thermal aging.
Barrier
Copper traces exposed to molten tin dissolve at rates exceeding one micrometer per second during standard soldering. Intermetallic compound layers form immediately at this liquid-solid boundary, creating the chemical bond that holds surface mount components to the circuit board. Solder joints operating above one hundred degrees Celsius experience continuous solid-state diffusion that thickens this interface over thousands of operating hours.
Without an engineered metallic partition between the base laminate copper and the tin-bearing alloy, that reaction consumes the conductive trace and replaces ductile metal with brittle crystalline phases.
Electroless nickel immersion gold deposits a phosphorus-doped nickel shell over the copper pad before assembly. Electroless nickel immersion gold plating prevents copper migration into SAC305 or SnPb solder pools during assembly reflow cycles. The nickel reacts with tin to generate Ni3Sn4 instead of copper-tin phases.
Ni3Sn4 grows at roughly one-third the speed of Cu6Sn5 under identical operating temperatures. Phosphorus content in the nickel deposit governs this barrier performance. Deposits containing six to nine percent phosphorus by weight yield an amorphous structure that resists tin penetration under continuous thermal stress.
Lower phosphorus concentrations create crystalline grain boundaries that accelerate diffusion pathways.
Intermetallic layers that grow too thick transform compliant joints into brittle fracture planes.
Electroless nickel electroless palladium immersion gold introduces a thin palladium cushion between the nickel and outer gold flash. The palladium layer measures between zero point zero five and zero point one five micrometers. Pure palladium dissolves into the solder alloy within two seconds of liquidus contact.
This dissolution leaves a ternary (Pd,Ni)Sn4 phase dispersed across the solder bulk rather than concentrated at the pad boundary. The resulting interface retains a thin, uniform nickel-tin compound that inhibits catastrophic interfacial fracture during mechanical shock events.
Solder Finish Metallurgy under Continuous Heat
Pad metallurgies respond differently when exposed to temperatures exceeding one hundred and twenty-five degrees Celsius. Immersion tin finishes create Cu6Sn5 compounds during storage prior to component placement. Subsequent thermal exposure in service converts this compound into Cu3Sn, depleting the underlying copper pad and forming microscopic separations.
Organic solderability preservatives leave bare copper directly exposed to solder alloys, permitting unrestrained copper dissolution during successive reflow passes.
Palladium additions alter the thermodynamic driving force of the tin-nickel reaction. The resulting quaternary intermetallic structures show reduced atomic vacancy formation at elevated operating temperatures. Component terminations plated with pure matte tin accelerate compound development when soldered onto bare copper finishes.
Solder balls containing bismuth or antimony alter diffusion constants across the joint interface.
| Phase Structure | Crystal System | Hardness (GPa) | Growth Rate Constant (m²/s) | Fracture Toughness (MPa·m½) |
|---|---|---|---|---|
| Cu6Sn5 (η-phase) | Monoclinic / Hexagonal | 6.2 to 6.8 | 2.8 × 10⁻¹⁷ | 1.12 |
| Cu3Sn (ε-phase) | Orthorhombic | 5.8 to 6.4 | 1.4 × 10⁻¹⁷ | 0.88 |
| Ni3Sn4 | Monoclinic | 7.1 to 7.9 | 8.5 × 10⁻¹⁸ | 0.94 |
| (Cu,Ni)6Sn5 | Hexagonal | 7.4 to 8.2 | 1.9 × 10⁻¹⁷ | 1.25 |
| (Pd,Ni)Sn4 | Orthorhombic | 5.2 to 5.9 | 6.1 × 10⁻¹⁸ | 1.05 |
Grain boundaries provide fast diffusion paths. When specifying board surface finishes for harsh environments, manufacturing documents must define layer thicknesses with explicit tolerances rather than nominal values. A nickel deposit thinner than three micrometers risks complete consumption over a five-year deployment at one hundred and twenty-five degrees Celsius.
Conversely, gold layers exceeding zero point zero eight micrometers generate AuSn4 needles within the bulk solder. Gold embrittlement creates shock vulnerability under drop conditions.
- Immersion Silver Finish transfers bare copper directly to the solder joint without an intervening diffusion barrier, accelerating Cu3Sn growth during thermal storage.
- Standard ENIG Coating provides reliable diffusion resistance provided phosphorus concentrations remain strictly between seven and nine percent by weight.
- ENEPIG Metallization arrests copper consumption through its intermediate palladium layer while preventing black pad corrosion defects during board fabrication.
- Direct Immersion Gold eliminates galvanic nickel attack entirely but permits rapid nickel leaching into high-temperature SAC alloys during rework.
Pure nickel dissolves at measurable rates. When selecting protective platings, thicker barriers delay copper consumption until the service life expires.
Profile
Thermal settings during convection reflow determine the starting thickness of the intermetallic layer before an assembly leaves the factory floor. Liquidus dwell time controls atomic dissolution rates between liquid solder and the solid substrate finish. Keeping liquidus duration between forty-five and sixty seconds produces an initial intermetallic compound thickness between zero point five and one point two micrometers.
Extending dwell duration past ninety seconds doubles this initial intermetallic layer, expending a large portion of the assembly thermal budget during the first minutes of manufacture.
Reflow peak temperatures dictate initial thickness. Peak temperatures exceeding two hundred and forty-five degrees Celsius for lead-free alloys such as SAC305 accelerate copper and nickel dissolution exponentially. Excessive thermal input produces scalloped, irregular Cu6Sn5 crystals with deep troughs between grains.
These valleys trap unreacted flux residues and create stress concentrators that initiate cracks under mechanical strain. A peak temperature between two hundred and thirty-five and two hundred and forty degrees Celsius creates planar, continuous intermetallic morphologies that distribute mechanical loads evenly across the joint area.
Solder joints exposed to two hundred and sixty degrees Celsius for sixty seconds develop an initial intermetallic layer between one point two and one point eight micrometers thick.
Cooling rates directly alter the final grain morphology. Rapid cooling between two and four degrees Celsius per second forces solder constituents to solidify quickly, suppressing secondary intermetallic coarsening. Slow cooling below one point five degrees Celsius per second allows extensive Ag3Sn plate growth in SAC alloys.
These large silver-tin plates act as crack propagation paths across the bulk joint. Nitrogen atmospheres containing less than fifty parts per million oxygen improve wetting spread while reducing necessary peak temperatures by five degrees Celsius.
Double-Sided Assembly Thermal Penalties
Passing a printed circuit board through the oven a second time exposes primary side joints to elevated liquidus temperatures. Bottom-side components experience temperatures near or above the alloy melting point, driving additional intermetallic compound expansion. A third pass destroys the barrier.
Heavy copper inner layers act as thermal sinks, drawing heat unevenly and forcing line operators to extend dwell times to ensure thorough solder melt on ground pads.
| Alloy Formulation | Melting Point (°C) | Target Peak Temp (°C) | Time Above Liquidus (s) | Initial IMC Thickness (µm) |
|---|---|---|---|---|
| Sn96.5Ag3.0Cu0.5 (SAC305) | 217 to 220 | 238 to 242 | 50 to 65 | 0.7 to 1.1 |
| Sn99.3Cu0.7 (Sn100C) | 227 | 245 to 250 | 55 to 70 | 0.8 to 1.3 |
| Sn63Pb37 | 183 | 210 to 215 | 45 to 60 | 0.4 to 0.8 |
| Sn95.5Ag3.8Cu0.7 (SAC387) | 217 | 240 to 245 | 60 to 75 | 0.9 to 1.4 |
| Sn90Bi10 | 138 to 210 | 225 to 230 | 50 to 60 | 0.5 to 0.9 |
Selective soldering of through-hole pins imposes localized heat shocks on adjacent surface-mount pads. Nozzle dwell times exceeding three seconds heat nearby solder joints to two hundred degrees Celsius through lateral laminate conduction. This localized heat drives solid-state intermetallic growth in adjacent components without complete reflow melting.
The resulting unrefined crystalline structures show reduced shear strength compared to primary reflow bonds.
Process engineers frequently claim that extended dwell times are mandatory to avoid solder voiding on large thermal pads.
Void
Vacancies within crystalline lattices coalesce into microcavities when unequal diffusion rates exist across a metallic interface. In copper-tin couples, copper atoms migrate into the solder matrix substantially faster than tin atoms diffuse into the copper substrate. This imbalance leaves an excess of atomic lattice vacancies along the substrate boundary.
When assemblies operate continuously above one hundred and twenty-five degrees Celsius, these vacancies aggregate into planar defects known as Kirkendall voids.
Kirkendall microvoids coalesce along the copper interface long before electrical discontinuity registers on an automated test fixture. As Cu6Sn5 transforms into thermodynamically stable Cu3Sn, molar volume decreases by roughly eight point five percent. This volumetric shrinkage generates intense localized tensile stresses.
If the parent copper foil contains excessive electroplating brightener residues such as sulfur, chlorine, or carbon, these impurities segregate at the Cu3Sn to copper interface. The combination of impurity segregation, lattice shrinkage, and unbalanced atomic diffusion creates a perforated separation plane along the pad surface.
How Do Elevated Operating Temperatures Accelerate Interfacial Degradation?
Thermal activation drives solid-state atomic diffusion according to the Arrhenius relationship. The growth rate of intermetallic layers follows parabolic kinetics governed by time and temperature exposure. At room temperature, copper-tin diffusion remains negligible over decades of storage.
When operational environments reach one hundred and fifty degrees Celsius, diffusion coefficients multiply by three orders of magnitude. The table below illustrates the kinetic shift across common automotive and industrial operating envelopes.
| Operating Temperature (°C) | Diffusion Constant D (m²/s) | Cu3Sn Growth (µm / 1000h) | Total IMC Thickness (µm / 1000h) | Kirkendall Void Area Fraction (%) |
|---|---|---|---|---|
| 85 | 1.2 × 10⁻¹⁹ | 0.08 | 0.45 | < 0.5 |
| 105 | 8.4 × 10⁻¹⁹ | 0.22 | 0.92 | 1.2 |
| 125 | 4.6 × 10⁻¹⁸ | 0.58 | 1.85 | 4.8 |
| 150 | 2.8 × 10⁻¹⁷ | 1.45 | 3.60 | 14.5 |
| 175 | 1.4 × 10⁻¹⁶ | 3.20 | 6.90 | 32.0 |
Intermetallic growth consumes the underlying copper trace until the conductive path thins dangerously. When an assembly utilizes standard half-ounce copper foil with an initial thickness of seventeen point five micrometers, continuous exposure to one hundred and fifty degrees Celsius consumes over five micrometers of parent metal within three thousand operating hours. This copper loss increases trace resistance while weakening the mechanical anchor between the solder joint and the glass-epoxy substrate.
Nickel depletion leaves the pad unprotected. On electroless nickel finishes, phosphorus does not dissolve into the Ni3Sn4 intermetallic layer. The nickel atoms migrate into the solder, expelling phosphorus back toward the unreacted nickel deposit.
This mechanism forms an amorphous, phosphorus-rich Ni-P layer containing twelve to fifteen weight percent phosphorus. This brittle zone, commonly called the black pad degeneration band, features low fracture toughness. Under continuous heat, nickel atoms continue their outward migration, creating Kirkendall microvoids directly inside this phosphorus-rich layer.
- Initial Phase Nucleation generates scallop-shaped Cu6Sn5 crystals at the liquid solder interface during convection reflow soldering, establishing the primary bond.
- Solid-State Transformation consumes tin from the bulk solder and copper from the pad during thermal operation, nucleating the planar Cu3Sn phase between the base copper and Cu6Sn5.
- Atomic Vacancy Supersaturation develops inside the Cu3Sn layer because copper diffusion rates exceed tin diffusion flux across the interface.
- Cavity Aggregation collects microscopic vacancies along the Cu3Sn to copper boundary, forming discrete microvoids visible under scanning electron microscopy at two thousand times magnification.
- Coalescence and Delamination merges individual microvoids into continuous sub-surface planar fissures that detach the solder joint completely during modest mechanical shock or vibration events.
Brittle fractures follow the copper interface. When thermal aging surpasses five thousand hours at one hundred and fifty degrees Celsius, shear resistance drops by more than sixty percent compared to as-built baseline values. Vibration regimes that are harmless to freshly soldered boards cause rapid fatigue failure along these degraded interfaces.
Field assemblies fail without prior electrical warning as microcracks sever the remaining metallic bridges across the void plane.
Thermal cycling drives rapid void coalescence. Assemblies failing from interfacial voiding produce catastrophic field warranty campaigns that scrap entire controller inventories.
Shear
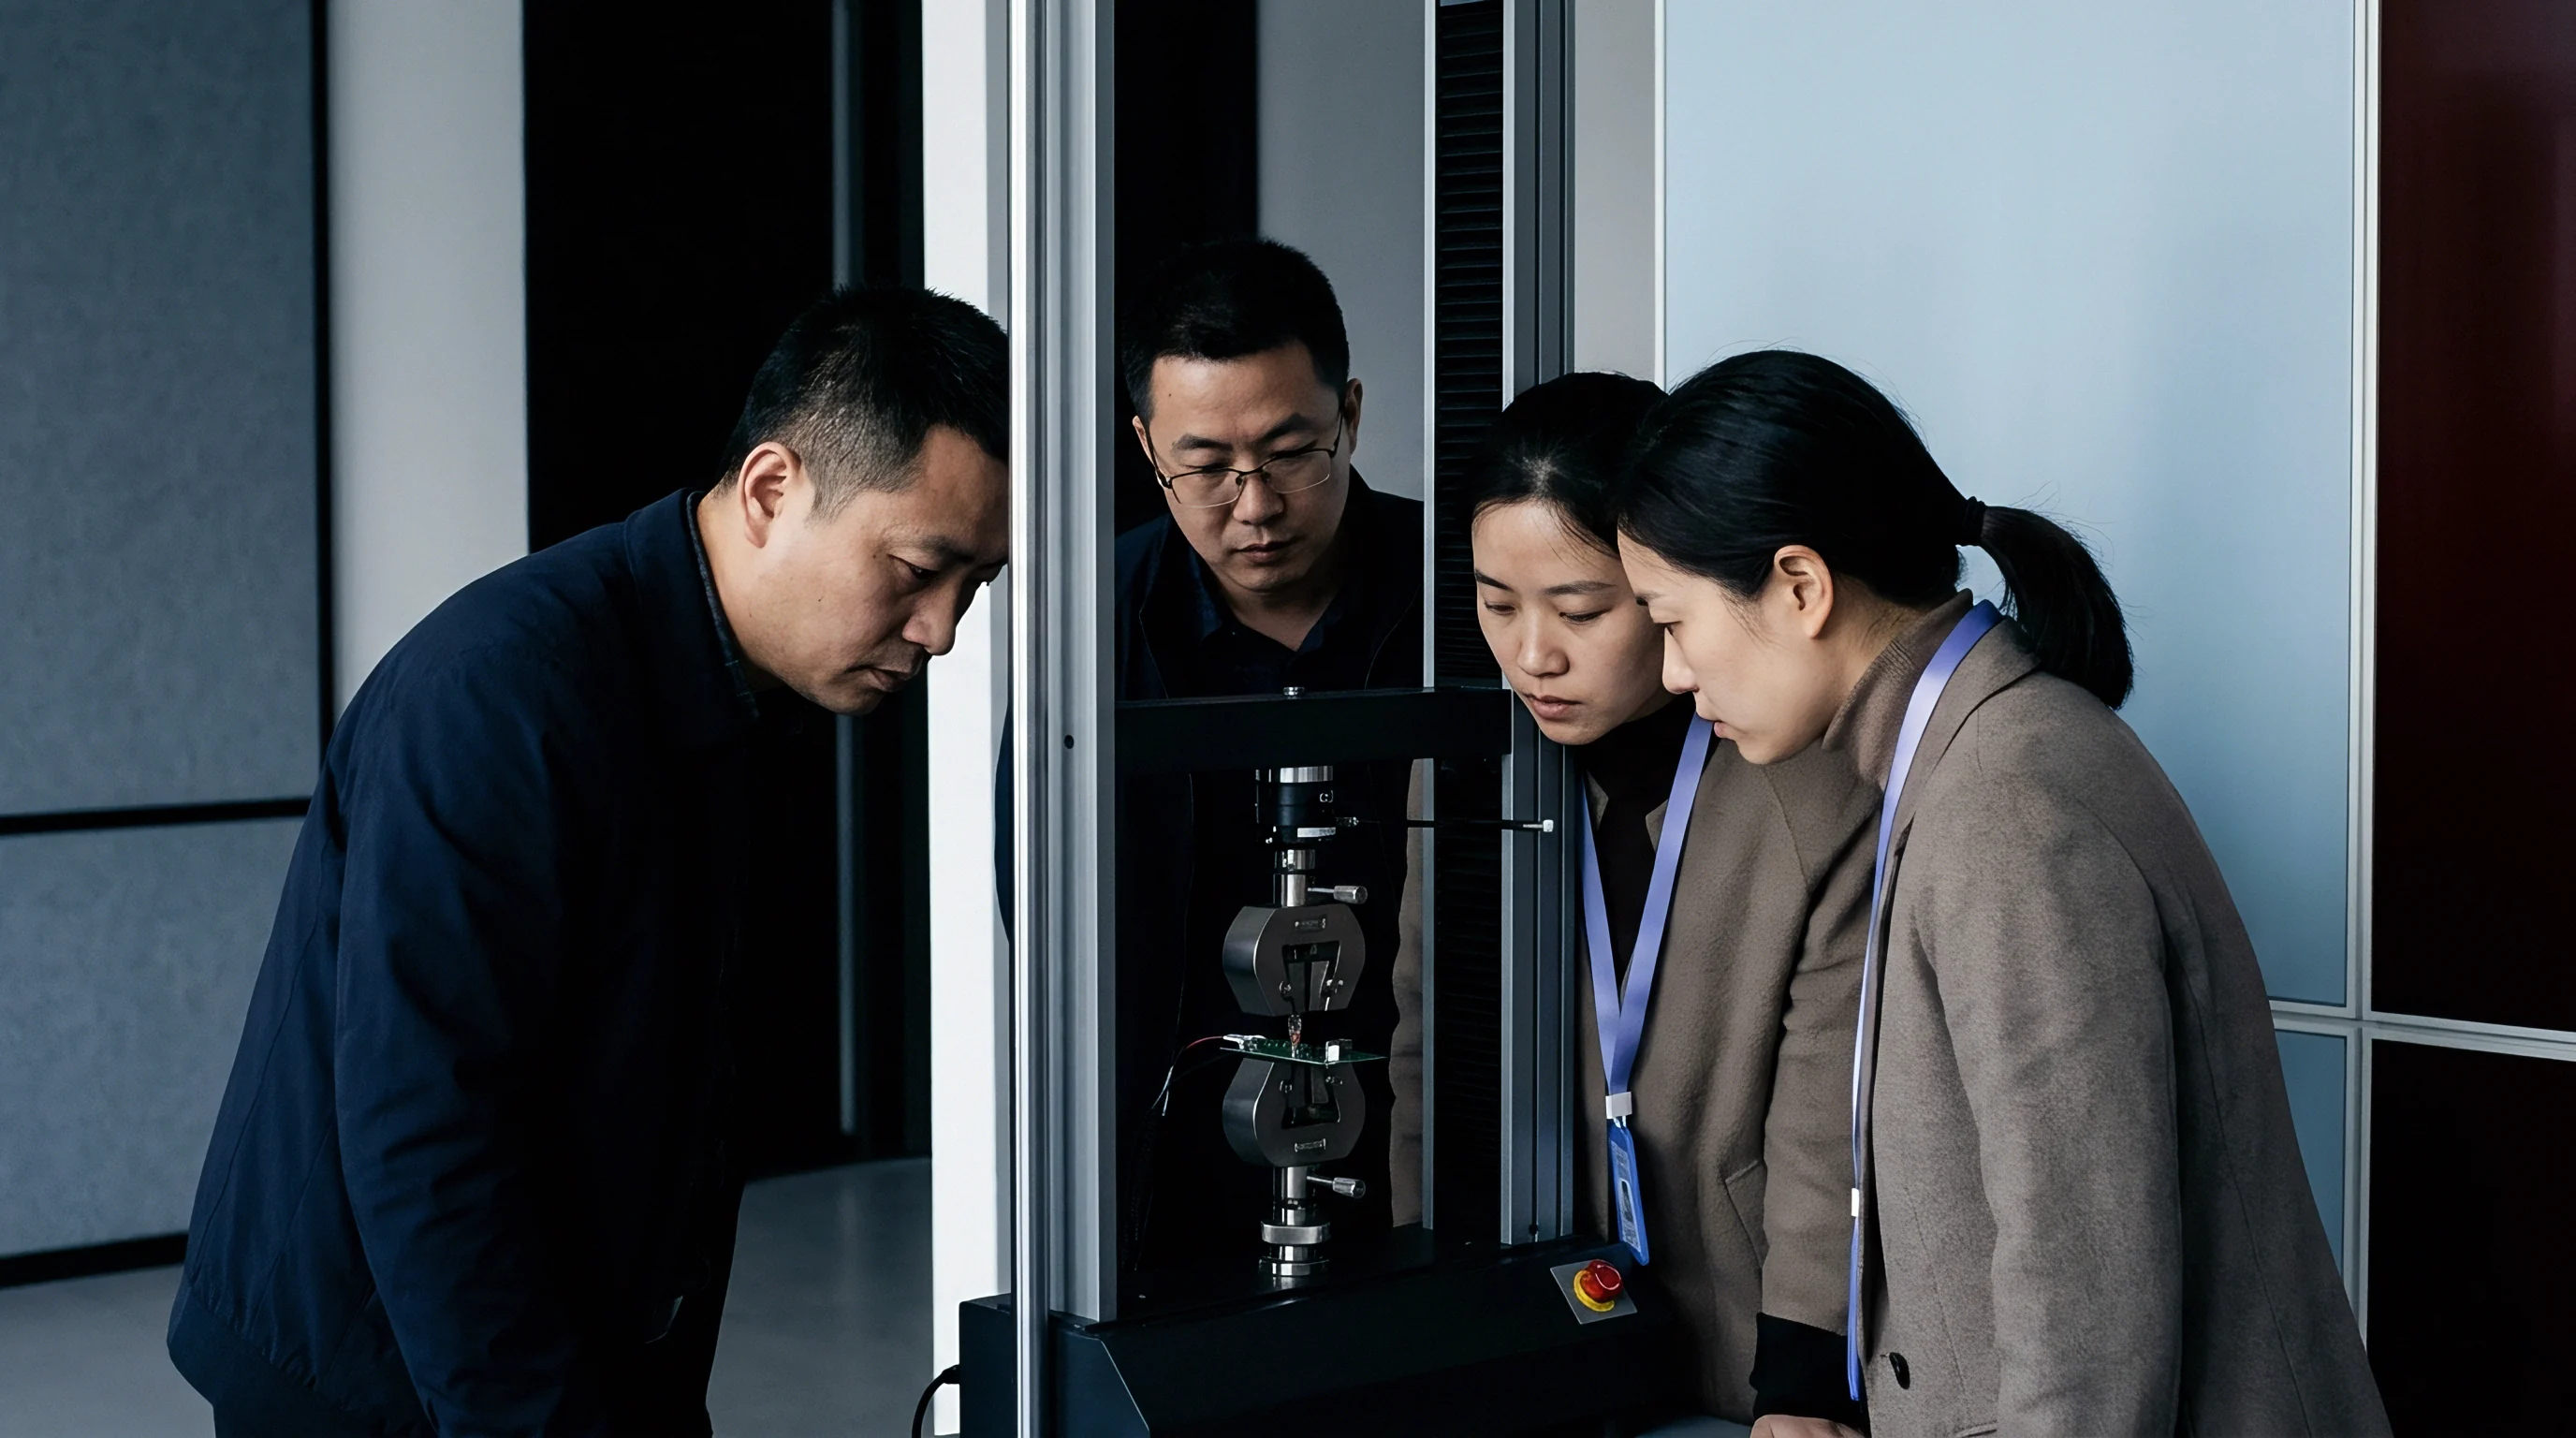
Mechanical verification validates whether intermetallic compounds have degraded beyond acceptable structural thresholds. Cold bump pull and high-speed solder ball shear testing measure the mechanical integrity of aged interconnects. Standard low-speed shear testing performed at zero point one millimeters per second yields misleading data because plastic deformation of bulk solder absorbs mechanical energy.
High-speed ball shear conducted between one hundred and five hundred millimeters per second transfers load directly to the intermetallic boundary, exposing interfacial brittleness and Kirkendall void networks.
Inspectors reject lots exceeding two micrometers. High-speed ball shear testing on SAC305 interconnects subjected to isothermal bake at one hundred and fifty degrees Celsius reveals a shift in fracture mode. Unaged joints demonstrate ductile failure through the bulk solder ball, leaving intact alloy across the pad.
Aged joints containing thick intermetallic layers transition to brittle cleavage fracture at the pad boundary. The fracture surface follows the interface between Cu3Sn and base copper or within the phosphorus-rich Ni-P layer.
Microsection Surveillance and Phase Measurement
Metallographic cross-sectioning remains the decisive analytical method for qualifying interfacial evolution. Technicians mount printed circuit board coupons in room-temperature curing epoxy to prevent artificial intermetallic expansion from mounting heat. Automated polishing down to zero point zero five micrometer colloidal silica reveals the multi-phase boundary without smearing ductile tin over brittle compound crystals.
Etching polished mounts with a four percent nitric acid in ethanol solution differentiates Cu6Sn5 from Cu3Sn under light microscopy.
| Test Method | Governing Standard | Target Parameter | Acceptance Threshold | Failure Indicator |
|---|---|---|---|---|
| High-Speed Ball Shear | JESD22-B117 | 100 to 500 mm/s | > 250 mN per ball | Brittle pad cleavage > 10% |
| Cold Bump Pull | IPC-9708 | 5 to 50 mm/s | > 180 mN per bump | Pad cratering or IMC split |
| Isothermal Bake Aging | JESD22-A103 | 150°C for 1000 hrs | IMC thickness < 4.0 µm | Continuous Kirkendall line |
| Scanning Electron EDX | ASTM E1508 | Phase stoichiometry | Cu:Sn ratio 6:5 and 3:1 | Ternary phase segregations |
Energy-dispersive X-ray spectroscopy confirms atomic composition across the joint cross section. Scanning electron microscopy linescans track copper, nickel, tin, and gold concentrations along the diffusion gradient. Testing stops after one thousand cycles.
When inspecting incoming production lots, cross-sectional evaluation must document total intermetallic thickness across ten randomly selected solder joints per production panel. Thickness measurements must average five distinct points per joint interface to account for crystalline irregularity.
The factory absorbs those scrap fees. Production audits reveal that board suppliers frequently substitute lower-cost electroplating chemistry that increases organic codeposition on copper foils. This substitution accelerates Kirkendall void generation under subsequent thermal exposure.
Validating raw board pad purity through secondary ion mass spectrometry identifies carbon, sulfur, and chlorine impurities prior to surface mount placement.
Does non-destructive acoustic micro-imaging possess sufficient axial resolution to identify Kirkendall microvoid bands before mechanical separation occurs?
Clause
Procurement agreements must define strict metallurgical limits rather than relying on generic workmanship standards. Commercial supply contracts for high-temperature electronics frequently reference IPC-A-610 for general assembly acceptance. IPC-A-610 requires evidence of wetting and an intermetallic bond, but it omits quantitative maximum thickness limits for intermetallic compounds after multiple reflow passes or extended burn-in cycles.
Relying on this standard permits suppliers to deliver assemblies whose thermal budgets were exhausted during excessive factory rework.
Purchase orders must specify IPC-7095 Class 3 criteria for ball grid array assemblies deployed in high-reliability applications. Contracts must require suppliers to retain metallographic coupons from every production batch for five years. The procurement agreement must state that total intermetallic compound thickness across the primary pad interface shall not exceed one point five micrometers in the as-soldered condition.
When contracts enforce these specific thresholds, suppliers adjust oven recipes and prevent unauthorized manual soldering passes.
IPC-7095 Table 5-1 sets maximum acceptable intermetallic thickness boundaries that trigger automatic lot quarantine when exceeded during incoming microsection audits.
Commercial clauses must mandate isothermal aging testing on pilot production runs. The supplier must subject five assembled boards per pilot build to one thousand hours of storage at one hundred and fifty degrees Celsius in accordance with JESD22-A103 Condition D. Following thermal bake, metallographic microsections must show less than four micrometers of total intermetallic compound growth. Furthermore, cross-sections must exhibit a Kirkendall void line density of less than ten percent along the copper interface.
The thermal budget resets after rework. Manual hand soldering with conventional irons delivers uncontrolled thermal energy into adjacent traces. Contracts must limit localized component rework to a single cycle using calibrated hot-gas rework stations running verified thermal profiles.
Replacement components must receive fresh solder deposits rather than reusing existing pad alloys. Every rework event must be logged in the unit serial record with operator identification, nozzle profile number, and dwell duration.
Section 7.3 of the Master Supply Agreement mandates that any production batch showing average intermetallic compound thickness exceeding two micrometers at final factory inspection faces immediate lot rejection, requiring the vendor to replace all affected boards at their sole expense.