Reconstructing Informal Production Line Deviations in Overseas Factories
Unrecorded line deviations bypass paper audits through manual tool tweaks and sensor jumps, requiring cycle telemetry and mass balance forensics to resolve.
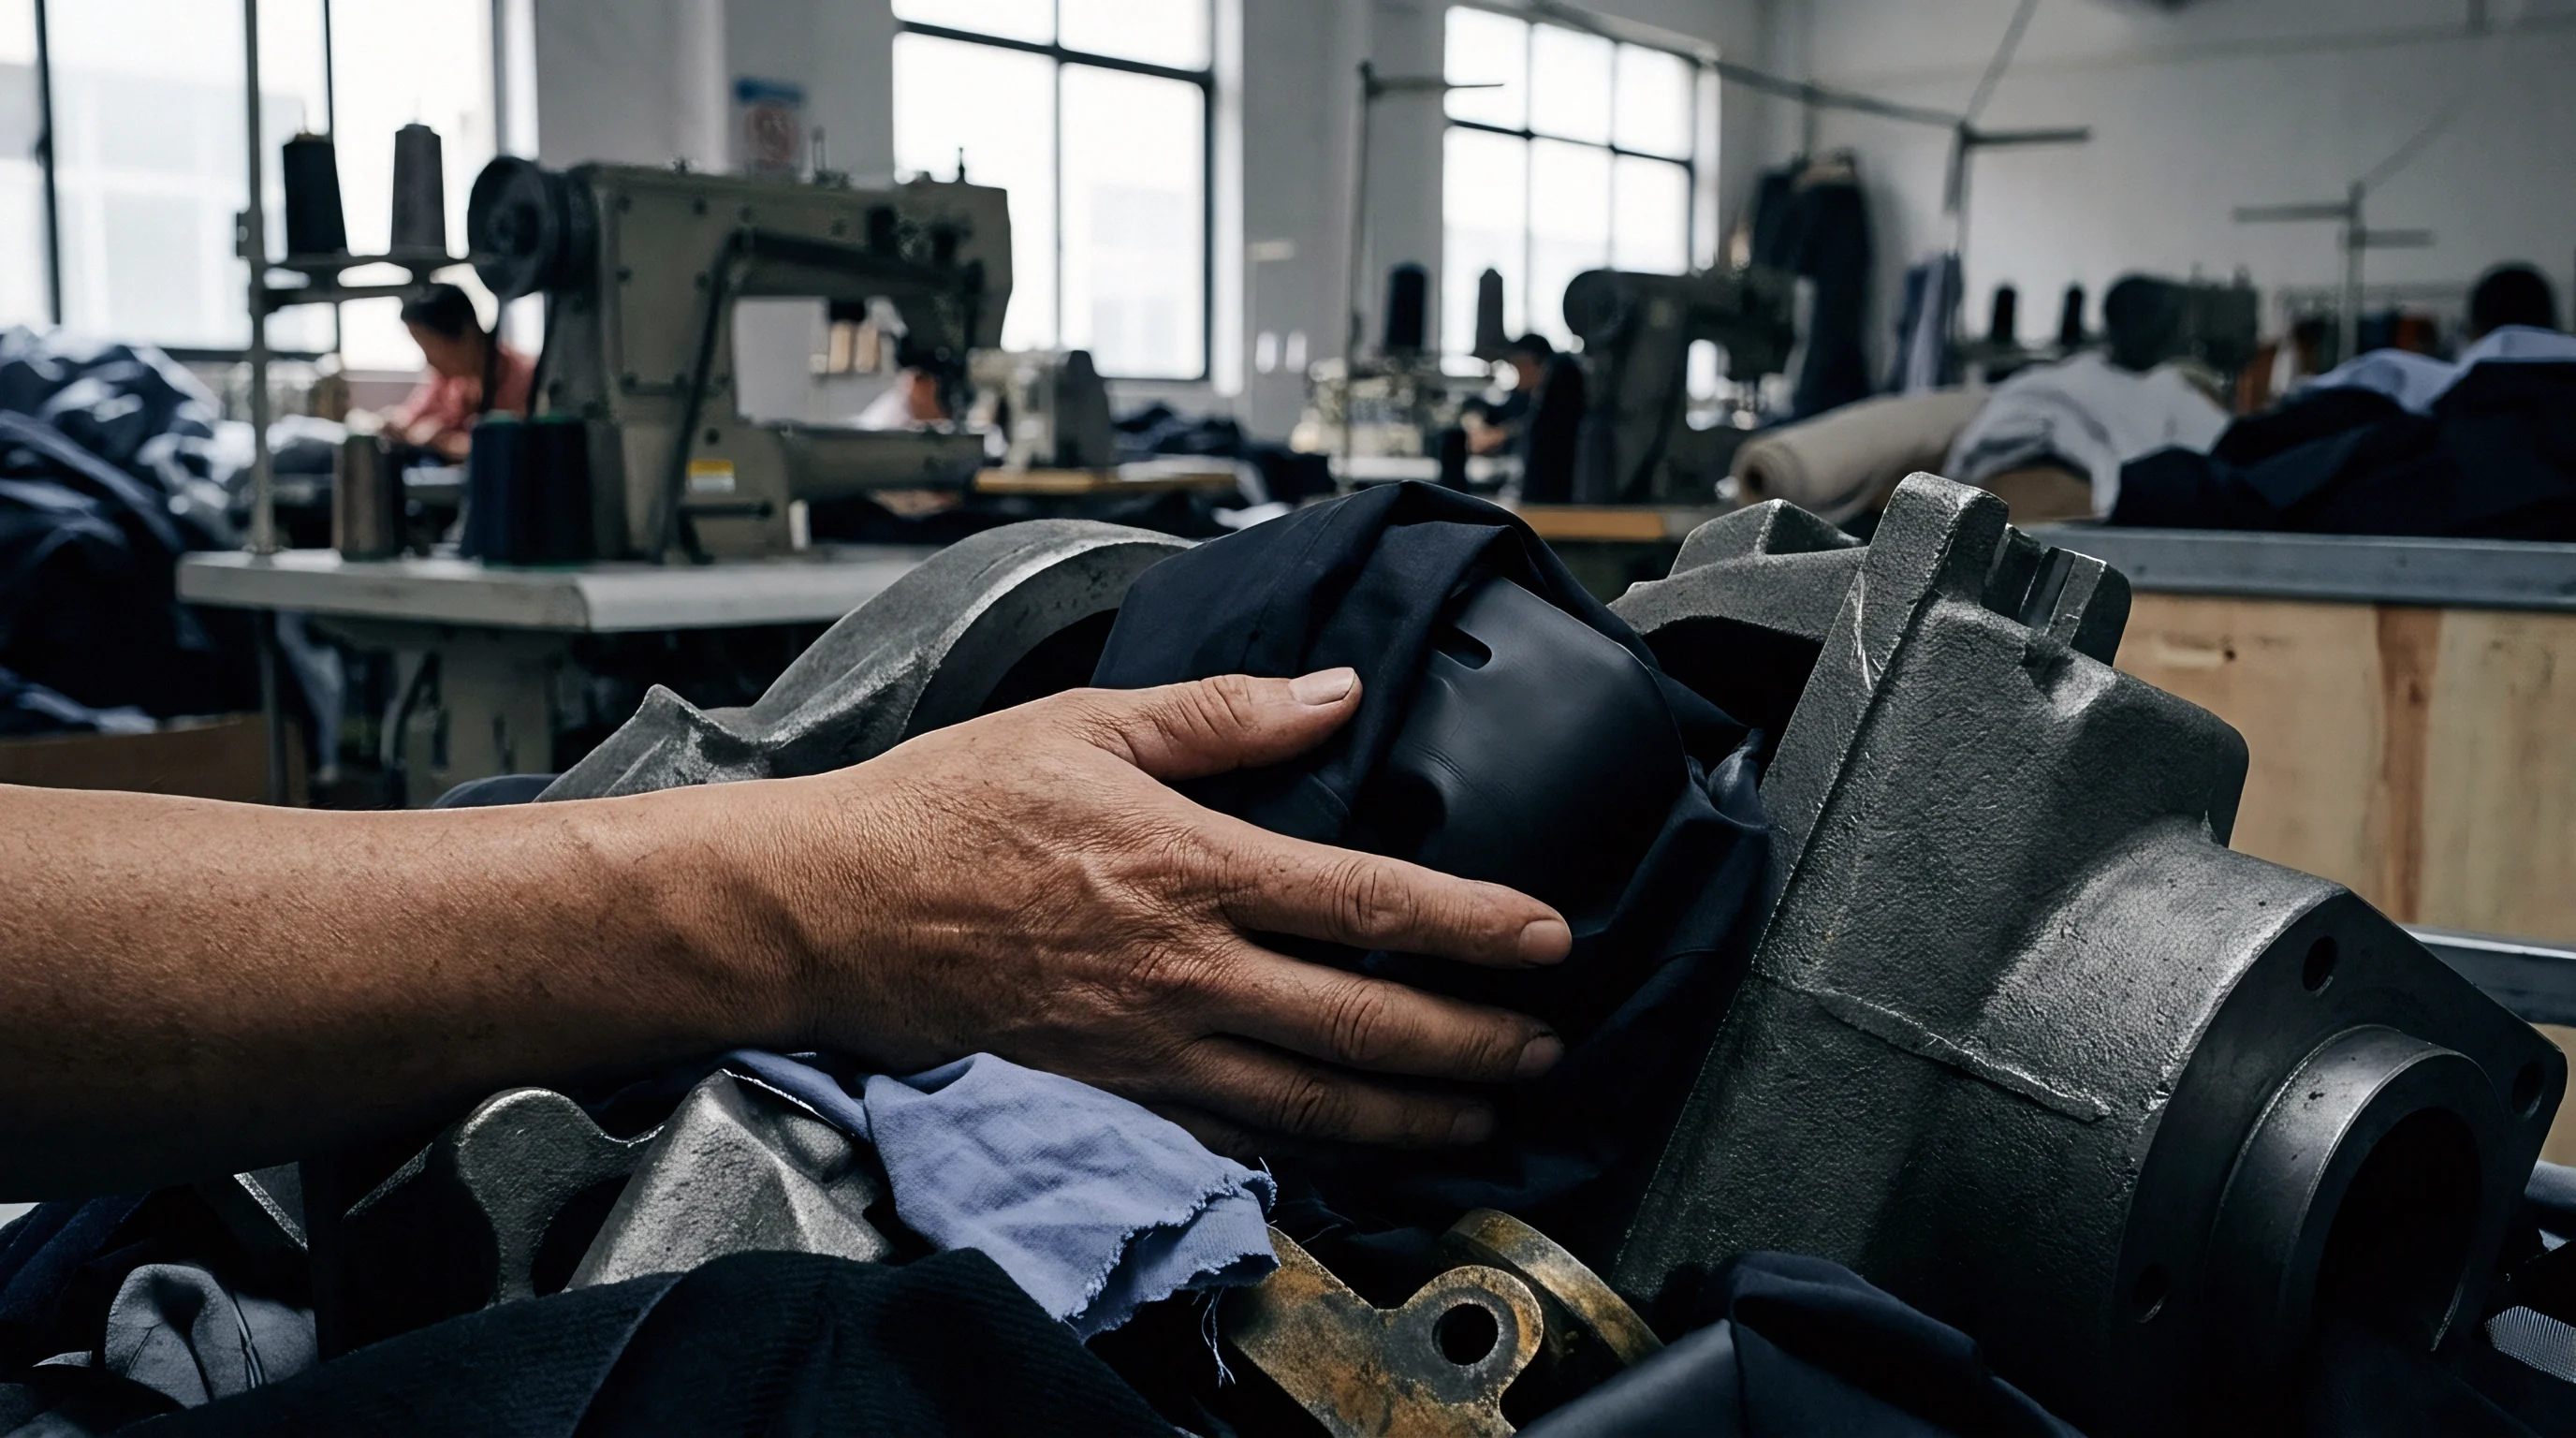
Floor
Morning shift operators at an assembly plant in Dongguan alter pneumatic press settings within ninety minutes of line start to meet piece-rate quotas. Line managers overlook the pressure gauge drop from 0.60 MPa to 0.42 MPa because output volume rises twelve percent. Engineering drawings call for continuous torque telemetry on stage four fasteners.
Workers substitute uncalibrated manual click-wrenches tucked behind yellow plastic totes when cycle times lag behind target tallies.
Informal deviations take root in the space between standard operating procedures posted in Chinese and the daily realities of production line incentives. Line supervisors balance daily ship quantities against scrap deductions assessed against team bonuses. When an automated ultrasonic welding horn runs twenty degrees hot, pausing for recalibration halts twenty workers downstream.
The line leader inserts a folded cardboard shim beneath the lower nest to compensate for thermal expansion. Production maintains nominal velocity while dimensional drift begins silently inside internal ultrasonic joints.
A fifteen-percent reduction in pneumatic line pressure drops joint shear strength below the threshold specified in ASTM D638 before the mid-shift break.
Reconstructing these undocumented interventions begins by examining the physical work cell rather than the official quality paperwork signed by the shift supervisor. The daily traveler card on station six records eighty-two compliant cycle sweeps. Physical examination tells a separate operational story:
- Scuffed clamp jaws indicate operators skipped soft-jaw polyurethane sleeves to accelerate component loading speeds during the morning changeover.
- Handwritten grease-pencil numbers on heating station frames override factory digital thermostat setpoints when ambient workshop temperatures fluctuate past thirty degrees Celsius.
- Secondary de-burring files stashed beneath conveyor rails reveal manual flash removal where worn injection tooling should trigger mold maintenance.
- Relocated safety interlock pins tied back with nylon zip ties allow technicians to cycle blister packaging stations without clearing jamming chutes.
Informal line modifications spread laterally across assembly workshops. When one team lead develops a bypass that prevents an automated screwdriving spindle from faulting on stripped bosses, adjacent line leads adopt the technique within two production shifts. Plant management rarely documents these adjustments in Engineering Change Orders (ECO).
The workshop foreman states that minor mechanical compensations keep components flowing without troubling the overseas design engineering office over inconsequential factory floor corrections.
Tuning
Assembly line adjustments originate in informal tooling tweaks made to mask upstream component variance without shutting down operational cells. Stamping blanks arriving from secondary vendors in Ningbo frequently exhibit three-hundred-micron thickness variations across single steel coils. When stamping dies bind, operators apply supplemental liquid drawing compound with domestic dishwashing sponges instead of adjusting press tonnage or flagging supplier batch defects.
Do Unauthorized Fixture Modifications Evade Standard Station Checklists?
Station checklists confirm that air hoses connect properly and power switches illuminate. They miss physical adaptations operators invent to smooth uneven component flow across aging fixtures. In a typical consumer electronics sub-assembly cell, an operator faces an aluminum bracket that binds inside an anodized chassis pocket.
Machining tolerances stacked unfavorably during morning stamping. The operator uses a round file on the bracket corner to force seating within seven seconds, leaving raw exposed metal vulnerable to galvanic corrosion under salt spray exposure.
| Station Identifier | Informal Adjustment Observed | Immediate Cell Objective | Downstream Failure Signature |
|---|---|---|---|
| ST-02 Insertion | Cardboard shim under guide rail | Prevent plastic housing snag | Axial misalignment exceeding 0.45 mm |
| ST-05 Soldering | External flux bottle manual dip | Overcome surface lead tarnishing | Dendritic growth under IPC-A-610 Class 2 |
| ST-09 Ultrasonic | Timer shortened by 0.3 seconds | Increase hourly unit throughput | Hydrostatic leak test failure at 1.2 bar |
| ST-12 Fastening | Dual-cycle clutch trigger trick | Drive cross-threaded screw down | Boss tear-out during drop impact |
Tracing mechanical interventions involves inspecting physical tool wear patterns that standard audits ignore. Workbenches show telltale shiny patches where operators hammer parts against fixture edges to correct warpage. Jigs display filed-down locator pins that allow slightly oversized castings to register without tripping station sensors.
When an automated optical inspection (AOI) camera alarms repeatedly on component misalignments, operators widen acceptance boundaries directly on the controller screen using administrative passwords written on masking tape behind the monitor.
ISO 9001 Section 8.5.1 mandates controlled conditions for production, yet floor-level parameter changes escape formal oversight whenever digital override passwords remain visible on terminal cowlings.
Forensic engineering of unrecorded adjustments demands rigorous examination of production line waste receptacles and tooling lockers. Unofficial files, coarse abrasive cloth, unauthorized solvents, and custom wire hooks indicate that operators routinely manipulate baseline manufacturing operations to offset dimensional imperfections. Mechanical fixtures show the true tolerances of the workshop floor.
Scrap
Reject bins positioned beside manual stations contain direct records of unauthorized line modifications. Official scrap manifests logged into the enterprise resource planning (ERP) system rarely tally with physical component counts extracted from grey plastic tubs awaiting evening recycling disposal. The discrepancy between logged rejections and actual workshop waste pinpoints unrecorded floor-level experiments carried out during production shifts.
Whose Signature Validates Daily Process Parameter Sheets?
Floor supervisors sign process sheets in batches during the final ten minutes before shift handovers. Operators run thermal curing tunnels thirty degrees hotter than specification during late afternoons to reduce dwell time from forty-five minutes to twenty-eight minutes. This acceleration clears floor congestion before the night shift arrives.
The written traveler sheet shows flat ninety-degree temperature profiles across all ten operating zones.
Calculating the true yield loss exposes these hidden corrections. Consider an operational run of ten thousand die-cast enclosures passing through an overseas powder coating line. The following model illustrates material loss hidden by unrecorded rework loops:
| Process Stage | Theoretical Material Mass | Recorded Material Mass | Discrepancy Volume | Operational Cause |
|---|---|---|---|---|
| Raw Ingot Melting | 12,500 kg | 12,480 kg | 20 kg | Normal oxidation melt loss |
| High-Pressure Casting | 11,800 kg trimmed | 11,200 kg net | 600 kg | Unlogged runner scrap remelt |
| CNC Edge Milling | 10,400 kg parts | 9,750 kg parts | 650 kg | Manual re-clamping cut errors |
| Solvent Degreasing | 9,750 kg clean | 9,750 kg clean | 0 kg | Inline tank dwell completed |
| Powder Application | 10,150 kg coated | 9,920 kg coated | 230 kg | Manual sand-off of runs |
| Assumes A380 aluminum alloy, virgin ingot density 2.71 g/cm³, baseline nominal wall thickness 2.2 mm. | ||||
Recycled flash and unlogged runners get shoveled back into melting pots without temperature normalization or degassing treatments. Secondary ingot inclusion counts surge. Castings develop internal porosity that remains invisible until precision computer numerical control (CNC) machining breaks through subsurface pockets on critical sealing grooves.
- Audit incoming raw inventory weight tickets against warehouse outbound shipping passes to establish initial mass balance baselines.
- Count empty primer and solvent drums behind the chemical shed to verify chemical application volume against square meters of coated product.
- Weigh metal swarf barrels beside computer numerical control centers to detect excessive stock removal resulting from oversized cast blanks.
- Inspect rework staging corrals situated behind carton packing stations for products pulled off the line for heat-gun straightening.
Unrecorded rework loops shorten product lifespans while presenting clean factory acceptance data. A buyer who fails to monitor scrap bin volumes accepts latent thermal fatigue in structural components, generating product warranty claims that appear six months after overseas transit.
Telemetry
Programmable logic controllers (PLCs) log millisecond-level cycle intervals that disclose unauthorized alterations to line mechanics. Line technicians modify machine parameters locally to bypass cycle interlocks. They alter pneumatic clamp dwell times, turn down cooling delays, and disable pressure transducer handshakes.
While the operator ledger records unbroken adherence to validated parameters, PLC hard drive event logs register clear digital signatures of manual intervention.
Consider an automated adhesive dispensing cell where cycle time should consume eighteen seconds per sub-assembly. The dispensing tip moves along an intricate path, waiting three seconds at corner radiuses to deposit uniform bead heights of 1.2 millimeters. Reviewing internal machine logs often uncovers sudden step-downs in cycle duration to eleven seconds:
- Feed rate multipliers bumped from 100 percent to 140 percent via handheld maintenance teach pendants shorten cycle paths.
- Corner dwell settings reduced to zero milliseconds create adhesive starvation across critical environmental sealing edges.
- Purge routine intervals postponed from every twenty cycles to every four hundred cycles save primer fluid while allowing nozzle caking.
- Pressure fault tolerances widened from five percent to thirty percent suppress warning lamps triggered by viscous adhesive curing inside supply lines.
Event logs pulled directly from Omron or Siemens line controllers reveal parameter modifications within twenty-four hours of an unannounced shift speed-up.
Validating process stability across eight thousand miles requires independent data extraction. Technicians on the ground plug diagnostic readers into machine bus networks during off-shift periods to bypass filtered plant management portals. The raw ladder logic dump confirms whether safety interlocks and inspection sensors run in active states or remain shunted via software jumper bits.
Discrepancies between digital event timestamps and paper inspection reports indicate falsified quality checkpoints. A vacuum decay tester logs test completions at forty-second intervals, yet the daily production sheet registers one finished enclosure every twelve seconds. This mathematical mismatch proves that operators tested only one unit out of three while stamping travelers for the entire production lot.
What operational mechanism explains why factory leadership allows this telemetry divergence to persist across consecutive fiscal quarters?
Restitution
Contractual controls must reflect the forensic realities of undocumented assembly line modifications. Standard supply agreements rely on warranties and post-facto indemnification clauses that offer minimal leverage once shipments clear export customs in Shenzhen or Ningbo. Enforcing line integrity requires binding the supplier to unannounced raw telemetry audits, physical scrap balance reconciliations, and immediate stop-shipment triggers tied to process tampering.
Purchase orders stipulate approved production equipment lists, validated fixture drawings, and hard-locked controller software checksums. A buyer implements strict contractual penalties for unauthorized tooling modifications:
- Verify software cyclic redundancy check (CRC) values on all automated assembly stations during monthly site walkthroughs.
- Establish daily scrap mass balance reporting thresholds where unaccounted material variance exceeding two percent automatically halts outbound container dispatch.
- Require tamper-evident physical security seals on pneumatic regulators, temperature controllers, and optical sensor brackets across all manufacturing tiers.
- Conduct unannounced twilight shift inspections focusing on workstation waste containers, chemical replenishment ratios, and secondary rework benches.
Operating agreements incorporate precise language regarding parameter compliance. Under typical manufacturing master services agreements, Section 14.3 establishes that any unapproved alteration to fixture geometry, machine cycle timing, or operating temperature profiles constitutes a material breach that voids buyer payment obligations for the affected production lot.