Financial Risk Distribution from Unsanctioned Sub Tier Material Changes in Remote Manufacturing Operations
Unsanctioned sub-tier material shifts multiply landed defect costs elevenfold through sorting fees and downtime claims, demanding direct FTIR receiving assays and contractual retainage offsets to enforce liability.

Grain

Sub Tier Material Substitution Mechanics
Injection molders and casting foundries operating in secondary industrial zones frequently adjust raw material formulations to manage narrow gross margins. When primary contractors issue engineering drawings specifying virgin PBT with thirty percent glass fiber reinforcement, sub-tier compounders face an immediate incentive to introduce post-industrial scrap or off-spec regrind into the hopper. The resulting polymer blend alters crystalline structure, thermal expansion coefficients, and long-term creep resistance without changing surface appearance under visual inspection.
Material swaps happen deep in the supply chain long before components arrive at the primary assembly line. Secondary resin compounders regularly introduce ten to forty percent regrind into primary molding runs, treating the practice as standard thermal recycling. In die-cast aluminum components, secondary smelters similarly replace A380 ingot with scrap metal streams high in iron and zinc, which increases die friction and lowers fatigue strength in structural housings.
Municipal power rationing during peak summer electricity surges in coastal industrial clusters often drives these material changes. Molders running on backup diesel generators try to protect operating margins by cutting back on virgin resin purchases and substituting cheaper, uncertified masterbatches.
Polymer Regrind and Recycled Resin Ratios
Mechanical properties degrade systematically as regrind ratios exceed published engineering limits. Thermal stress testing shows that unannounced regrind additions immediately reduce tensile strength and heat deflection temperatures while accelerating environmental stress cracking under standard operational loads.
| Material Spec | Regrind Percentage | Tensile Strength Drop | Heat Deflection Shift | Impact Resistance Loss |
|---|---|---|---|---|
| PA66 GF30 | 10 Percent | 2.4 Percent | -1.8 Degrees C | 4.1 Percent |
| PA66 GF30 | 25 Percent | 8.7 Percent | -5.2 Degrees C | 14.3 Percent |
| PA66 GF30 | 40 Percent | 18.5 Percent | -12.6 Degrees C | 31.0 Percent |
| PBT GF30 | 15 Percent | 4.1 Percent | -2.5 Degrees C | 7.8 Percent |
| PBT GF30 | 35 Percent | 15.2 Percent | -9.8 Degrees C | 26.4 Percent |
The primary assembly plant receives sub-tier parts that pass initial dimensional checks while concealing structural flaws. For instance, a batch of connector housings molded with thirty-five percent regrind passes coordinate measuring machine checks at twenty degrees Celsius, yet fails dielectric retention tests as soon as field temperatures reach sixty degrees Celsius.
Sub-tier suppliers often defend unannounced resin adjustments as harmless process tweaks made to meet delivery schedules.


Cascade

Propagation across Supply Chains
Defective sub-tier components get built into higher-level assemblies, burying raw material failures beneath finished structural enclosures. Assembly workers drive screws into sub-tier housings using automated tools, causing micro-fractures along weakened screw bosses that double failure rates under load. The defect stays hidden until finished products undergo oceanic transit and the vibration cycles of domestic trucking.
A single unannounced polymer shift at a Tier-3 molder creates cascading operational losses downstream. The Tier-1 integrator builds ten thousand power electronics subassemblies around modified structural brackets, wasting labor, thermal paste, fasteners, and functional testing time on parts destined to crack prematurely in the field.
Differential Scanning Calorimetry shows a 2.4 Joules per gram enthalpy peak variance on 30 percent glass-filled Polybutylene Terephthalate tested under nitrogen at 10 degrees Celsius per minute when regrind content exceeds 15 percent.
Latent Thermal Degradation in Finished Subassemblies
Thermal cycling during standard burn-in testing accelerates structural fatigue in compromised materials. Brackets warp under continuous sixty-five degree operating environments, displacing surface-mount components and inducing trace fractures on adjacent circuit boards, which voids supplier warranties.
Downstream testing yields irregular fault codes that send engineering teams down electrical troubleshooting paths rather than toward raw material analysis. Technicians swap out perfectly good power MOSFETs while the underlying mechanical housing keeps distorting, multiplying diagnostic bench hours across production lots.
Unchecked material modifications deep within sub-tier operations turn minor unit savings into systemic product recalls across global distribution channels.


Sieve

Analytical Testing Methods at Receiving
Incoming quality control departments use analytical testing to intercept sub-tier substitutions before raw stock enters molding lines or assembly streams. Because standard dimensional tools cannot detect chemical composition changes in raw polymers or metal alloys, incoming inspection plans require laboratory equipment that can measure molecular mass shifts, drops in filler concentration, and secondary alloy contaminants.
- Sample three random containers from each incoming raw material consignment, isolating five hundred grams of material per container under controlled ambient humidity.
- Perform Fourier Transform Infrared Spectroscopy scans across the two hundred to four thousand wavenumber spectrum, comparing sample absorption peaks against the baseline golden sample fingerprint.
- Execute Differential Scanning Calorimetry heating runs from twenty to three hundred degrees Celsius at ten degrees per minute to determine melt point enthalpy and oxidation induction time.
- Measure Melt Flow Index under standard ASTM D1238 load conditions, recording melt flow rates against published material datasheet boundaries.
- Perform burn-off testing per ASTM D5630 to quantify inorganic glass fiber content, weighing residue on an analytical balance to four decimal places.
ISO 1043-1 material coding mandates full declaration of flame retardant additives and filler percentages, making unannounced formulation shifts an explicit breach of international material standards.
Differential Scanning Calorimetry and Spectroscopic Screening
Spectroscopic fingerprint matching identifies chemical substitutions within forty-five minutes of shipment arrival. Differential scanning calorimetry measures endothermic transitions, exposing blended polymers through broadened melting peaks and secondary glass transition shoulders.
Melt Flow Index testing gives an immediate indication of polymer degradation. A thirty percent increase in melt flow rate points to reduced molecular weight from excessive regrind cycles or thermal breakdown during compounding. Likewise, tensile testing of PA66 GF30 bars pulled from a twelve-tonne consignment under ASTM D638 conditions yields a 14.2 percent tensile modulus drop when moisture content stays below 0.02 percent, confirming structural alteration.
Estimating exact regrind ratios in glass-filled polymers from Melt Flow Index testing alone carries substantial analytical uncertainty: melt flow rates shifting between 8.5 and 14.1 grams per ten minutes can correspond to anywhere from fifteen to forty-five percent unrefined regrind depending on prior thermal history. Buyers handle this uncertainty by requiring FTIR fingerprint matching alongside melt flow data before accepting a lot.
Purchasing contracts that incorporate ISO 10204 Type 3.1 inspection certificates legally require the primary manufacturer to validate material chemistry through an accredited independent laboratory before clearing a lot.


Indemnity

Contractual Allocation of Sub Tier Material Risk
Commercial contracts determine which entity bears ultimate financial responsibility when sub-tier material alterations trigger downstream product failures. Master Service Agreements frequently include boilerplate clauses holding Tier-1 suppliers liable for all component performance, but enforcing those terms across international borders grows complicated when Tier-1 integrators operate on thin margins with few local assets.
Contractual indemnities must explicitly address sub-tier material integrity, defining unannounced raw material shifts as material breaches of specification rather than routine quality variance. Buyers retain leverage by inserting liquidating indemnity clauses into Purchase Order General Terms and Conditions.
| Contract Mechanism | Legal Coverage | Financial Recovery Limit | Enforcement Lead Time |
|---|---|---|---|
| Standard PO Terms | Direct Component Replacement | Direct Component Value | 30 to 60 Days |
| Bespoke MSA Indemnity | Rework, Sorting, Air Freight | 100 Percent Landed Defect Cost | 90 to 180 Days |
| Sub-Tier Pass-Through Clause | Tier-2 and Tier-3 Direct Liability | Bonded Sub-Tier Assets | 180 to 360 Days |
| Escrow Warranty Reserve | Immediate Defect Compensation | Deducted from Retention Pool | 1 to 5 Days |

Who Absorbs the Financial Impact of Unverified Resin Substitutions?
Financial liability defaults to the buyer when contracts lack explicit sub-tier audit rights and raw material change notification mandates. Overseas buyers who rely entirely on Tier-1 quality declarations end up absorbing sorting fees, air freight surcharges, and customer line-down penalties once defects surface in domestic markets.
Unsanctioned material modifications deep within sub-tier supply lines transform routine manufacturing variance into complete financial exposure for the primary importer of record.
Sub-tier pass-through agreements attempt to bridge this legal gap by binding Tier-2 molders directly to primary product specifications. Implementing them requires formal triangular contract structures among the buyer, the Tier-1 integrator, and the sub-tier compounder.
Legal enforceability ultimately rests on whether cross-border jurisdiction clauses permit effective asset seizure in the supplier’s home court.


Disbursement

Financial Risk Distribution Modeling
Distributing financial losses caused by sub-tier material changes requires tracking direct component costs alongside secondary operational expenses. Total landed defect costs encompass incoming inspection labor, laboratory diagnostic fees, line-down charges, global containment freight, manual sorting, scrapped components, and secondary manufacturing rerun hours.
Accounting for sub-tier failure costs demands an objective formula that assigns specific expenses to the party responsible for material validation. Buyers build cost-recovery models into financial settlement agreements to execute swift chargebacks against open purchase orders.

Worked Financial Allocation for Unsanctioned Polymer Swaps
To evaluate financial risk distribution, consider a production run of 100,000 structural enclosure units using glass-filled Polybutylene Terephthalate (PBT GF30) produced by a Tier-1 molder. The contract specifies virgin resin priced at $3.80 per kilogram, with each enclosure weighing 0.40 kilograms, bringing total virgin resin cost for the lot to $152,000.
If the Tier-2 compounder substitutes thirty-five percent regrind priced at $1.40 per kilogram without customer authorization, the sub-tier compounder saves $33,600 across the lot. That unsanctioned change degrades thermal resistance, triggering a 4.5 percent field failure rate once subassemblies experience operating stress inside finished electronics.
- Direct Material Scrap Loss calculated at 4,500 defective units scrapped at full manufacturing assembly cost of $18.50 per unit, generating $83,250 in unrecoverable physical product loss.
- Containment and Sorting Expense requiring 100 percent inspection of 95,500 remaining finished units across two domestic warehouse locations at a rate of $2.20 per unit, totaling $210,100 in manual sorting labor.
- Emergency Replacement Freight Costs air-freighting 4,500 replacement units from the overseas factory to the domestic assembly line to prevent complete factory shutdown at $8.60 per unit, adding $38,700 in logistics charges, which triples landed unit cost.
- Analytical Bench Diagnostic Fees conducting third-party FTIR, DSC, and mechanical testing across thirty lot samples to prove material breach for legal recourse, costing $14,500 in laboratory fees.
- Assembly Line Downtime Penalties covering twelve hours of idle downstream customer assembly line time assessed at $4,000 per hour, generating $48,000 in operational downtime claims.
The total landed cost of this unsanctioned material change reaches $394,550 against an initial sub-tier savings of $33,600 ~ a cost multiplier between sub-tier savings and landed loss exceeding eleven to one.
| Cost Category | Sub-Tier Savings | Landed Loss Amount | Tier-1 Recovery Potential | Net Importer Loss |
|---|---|---|---|---|
| Raw Material Swap | $33,600 | $0 | $0 | $0 |
| Scrapped Subassemblies | $0 | $83,250 | $83,250 | $0 |
| Warehouse Sorting | $0 | $210,100 | $105,050 | $105,050 |
| Air Freight Surcharge | $0 | $38,700 | $38,700 | $0 |
| Laboratory Testing | $0 | $14,500 | $14,500 | $0 |
| Line Downtime Claims | $0 | $48,000 | $0 | $48,000 |
| Total Financial Impact | $33,600 | $394,550 | $241,500 | $153,050 |
Recovering funds from Tier-1 integrators requires structured financial offsets applied against pending production invoices. Importers withhold payments on active shipments, using formal rejection notices to enforce contractual indemnity terms through immediate invoice deductions.
Contractual risk allocation formulas fail whenever chargeback calculations omit downstream warehouse sorting hours and secondary air freight surcharges from the baseline financial claim.
Effective financial risk distribution relies on maintaining a rolling retainage pool equal to ten percent of total monthly purchase order value until lot verification tests pass.
Dock

Receiving Protocols and Physical Containment
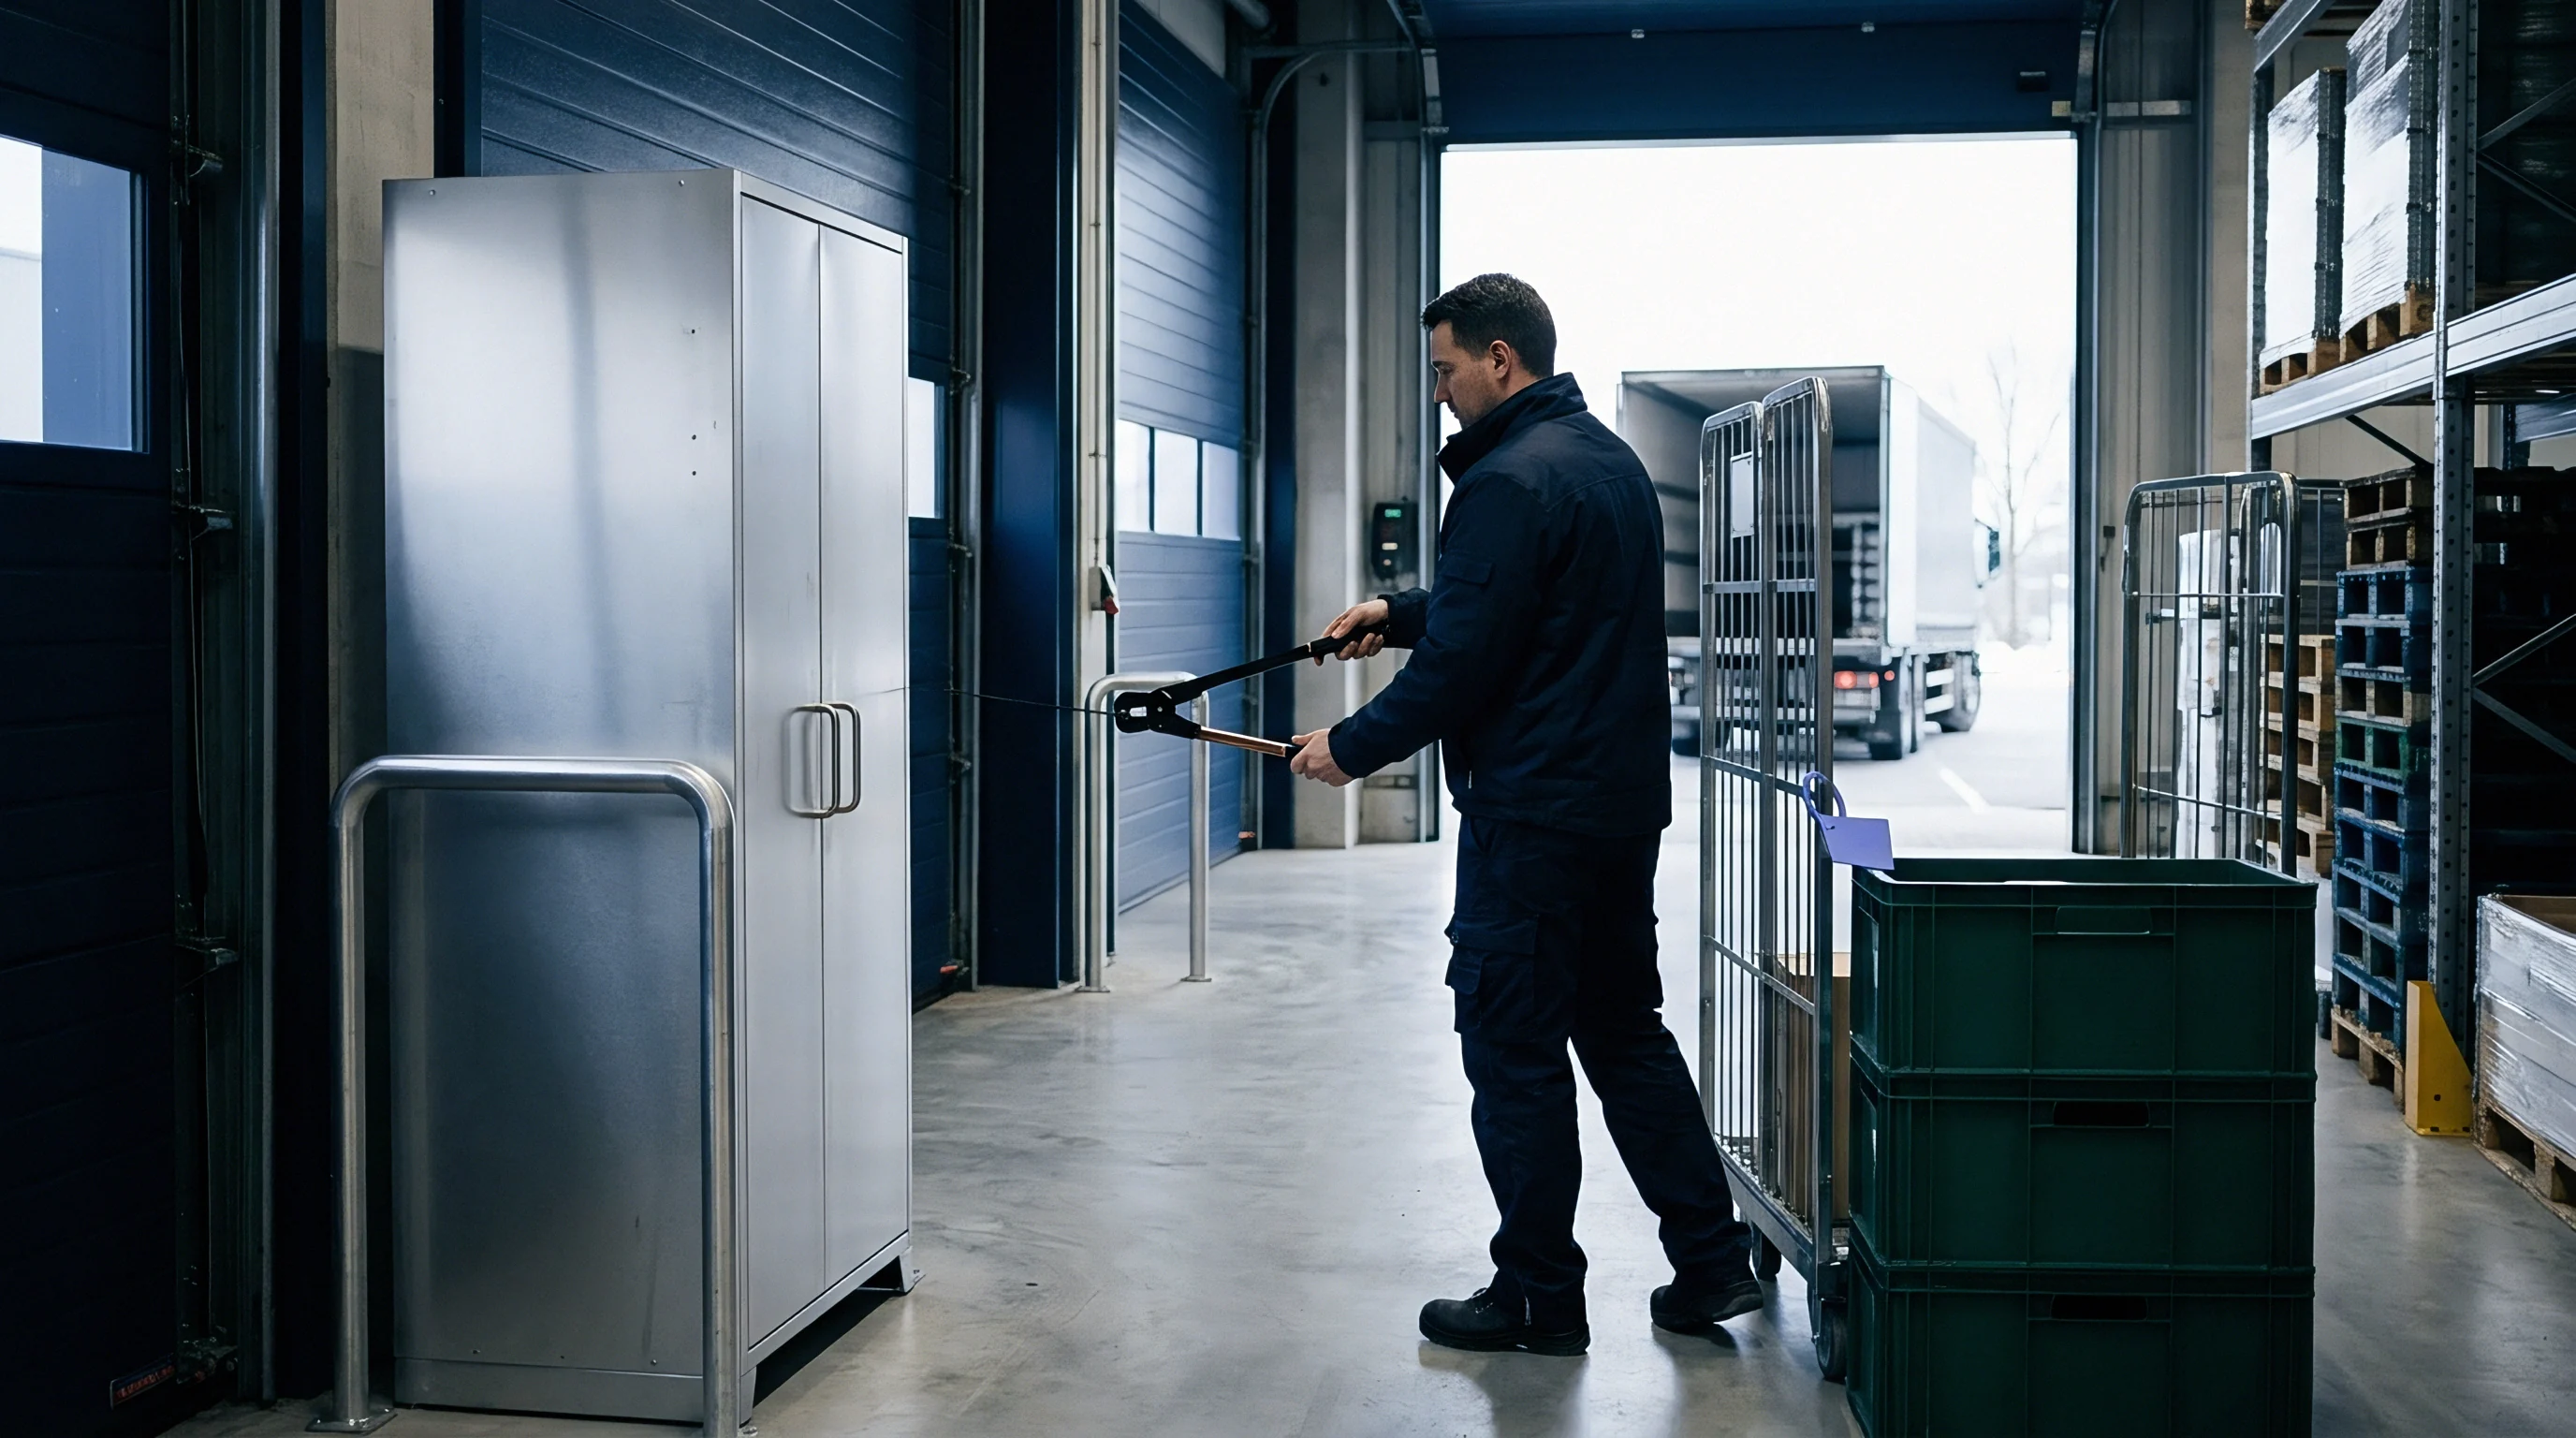
Receiving docks serve as the final physical barrier preventing unverified sub-tier components from entering active assembly streams. Quarantine procedures must halt suspicious consignments before receiving slips are signed, with warehouse teams placing incoming pallets into designated quarantine zones under physical locks and red containment tags until chemical testing confirms specification compliance.
- Quarantine Segregation Protocol isolates suspect shipments inside locked wire enclosures immediately upon offloading, preventing material handlers from moving unverified lots into primary manufacturing inventory.
- Traceability Label Verification matches sub-tier heat numbers and compound lot codes against factory certificates of analysis to verify continuous supply chain custody.
- Destructive Sampling Execution extracts five finished components from every twentieth pallet, routing samples directly to the chemical testing facility under strict chain-of-custody documentation.
- Logistics Hold Issuance notifies customs brokers and freight forwarders that pending shipments carry active commercial disputes, freezing transport payments until quality holds resolve.

Quarantine and Return Freight Allocation
Managing rejected goods requires early commercial agreement on return transport expenses and customs re-export declarations. Overseas suppliers often hesitate to authorize return shipping for rejected lots because of local import duties on returned manufactured goods; re-export documentation must explicitly cite raw material non-conformance to avoid duplicate export tariff assessments.
Physical custody of non-conforming materials stays at the receiving facility until the Tier-1 integrator posts financial collateral covering return freight and destruction fees. When international return freight costs exceed component scrap value, importers destroy defective parts locally and secure third-party destruction certificates to document asset liquidation for tax write-offs.
Standard commercial agreements require suppliers to collect rejected inventory within thirty business days of formal notice. Material remaining after thirty days becomes subject to local disposal fees assessed directly against open supplier payables.