Meaning
Cyclic exposure of test specimens to varying gas temperatures defines the methodology used for assessing hardware resilience against rapid climate variations during logistics and operations. In the context of manufacturing inside China, air to air thermal shock is a standard reliability test governed largely by GB/T 2423.22 specifications. This process subjects a component to alternating environments of extreme heat and extreme cold within a transition period that typically takes place in seconds.
The test measures the physical integrity of solder joints, seals and housing materials by inducing mechanical strain through differential expansion. It stops applying once the specified number of cycles completes or the material reaches a predefined point of catastrophic fracture. Validation protocols within Chinese supply chains often rely on this technique to simulate the environmental stressors found in northern industrial zones during winter shipment phases.
Transition Mechanism
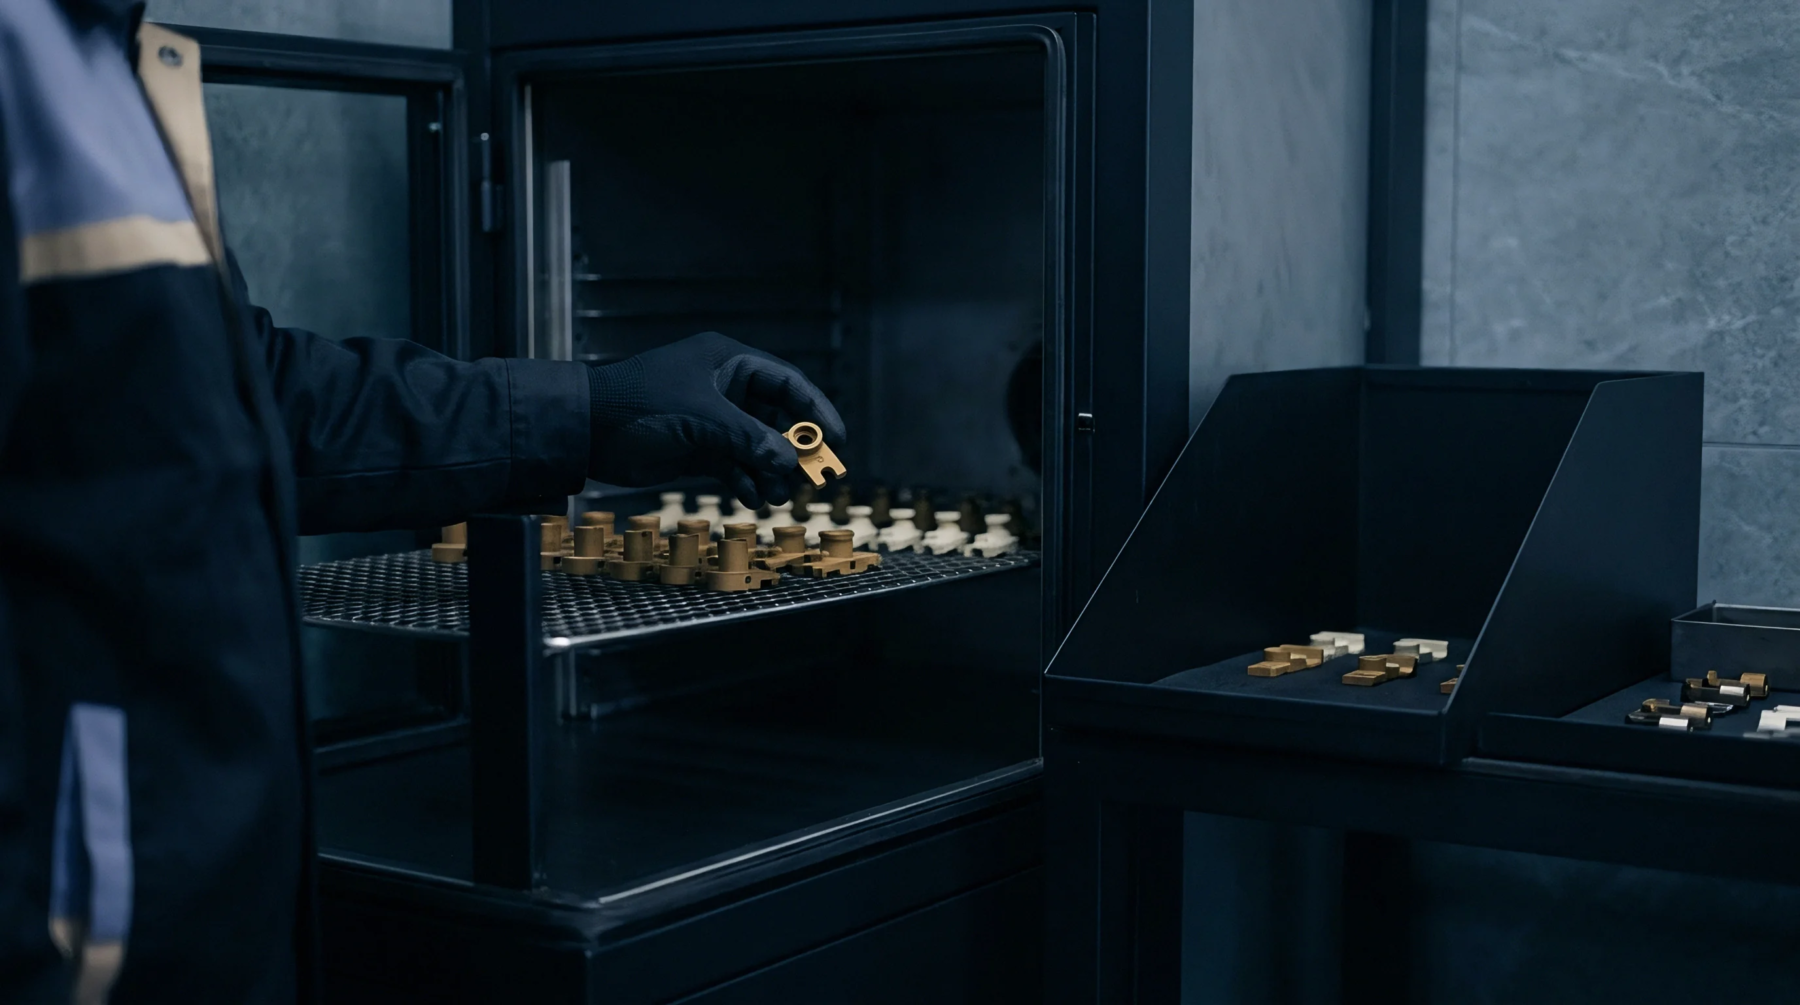
Heat transfer efficiency during the swap between chambers dictates the severity of the load applied to the assembly. Because air to air thermal shock moves the product between two stationary temperature zones, the air flow velocity across the sample surface directly influences how fast the internal temperature aligns with the target. The thermal mass of the carrier basket and the sample itself must be balanced against the heating or cooling power of the system to maintain a steep ramp rate.
If the mass is too high, the stress levels drop and the test fails to trigger the latent defects intended for discovery. High throughput facilities in the Pearl River Delta often employ dual chamber lifts that physically transport items between a preheated upper zone and a chilled lower zone. This mechanical movement must ensure stability so that vibration does not add an uncontrolled variable to the fatigue profile of the electronics.
When the dwell time starts, the internal sensors within the unit must confirm that the core temperature has saturated before the next transfer begins. If saturation is not reached, the test does not meet the jurisdictional quality requirements for tier one automotive grade certifications.
Fatigue Consequence
Failure to pass this rigorous cycle frequently manifests as delamination within the substrate or the cracking of hermetic seals in sensitive sensors. Since air to air thermal shock creates repeated expansion and contraction, the accumulation of microscopic stress leads to grain structure changes in metallic connections. Once a crack begins, subsequent cycles extend the breach until electrical continuity is lost.
In many Chinese production contracts, a single failure during this test necessitates a total review of the material selection or the reflow profile used in assembly. The financial risk is tied to the total lot size, as a failure in testing indicates a high likelihood of field returns across the entire batch. Successful completion proves that the assembly can withstand the rigors of maritime transport and fluctuating warehouse environments without degradation of internal logic or physical stability.
Operational Limit
Testing duration is governed by the saturation point of the test piece rather than an arbitrary hourly schedule. For very small components like surface mount capacitors, the air to air thermal shock cycles might take minutes to complete their full thermal swing. For larger industrial controllers or battery casings, the soak times expand significantly to allow the heat to reach the innermost geometries.
Limits on the applicability of this method appear when the air velocity required to drive the shift becomes high enough to cause acoustic or windage damage to the item under test. In these specific configurations, the thermal exchange is limited by the surface area of the component relative to its weight. If the target involves extreme miniaturization, researchers occasionally prefer liquid media to reach the desired intensity, yet for most consumer electronics, the gaseous exchange remains the statutory standard for acceptance.
Final approval for shipping requires data logging from every sensor to show that the prescribed profile was held without deviation from start to finish.