Detecting Unauthorized Factory Line Component Substitutions Early
Stop unapproved component swaps early by placing XRF plating checks at receiving, locking feeder software to the approved BOM, and auditing distributor manifests.
Triage
Incoming Freight Verification at Goods Inward
Reels of passives arrive with laser-etched markings that match an approved manufacturer part number while carrying internal dies sourced from uncertified domestic wafer lots. The physical packaging presents correct barcoding, factory heat seals, and legitimate outer distributor labels. Secondary distributors frequently repackage low-tier domestic clone semiconductors into re-taped carrier reels, presenting documentation that matches the approved bill of materials.
The assembly floor consumes these parts within hours of delivery if receipt checks rely entirely on barcode scanning and packing slips. Early detection requires moving component verification directly to the inbound receiving dock before components move into automated surface mount feeders.
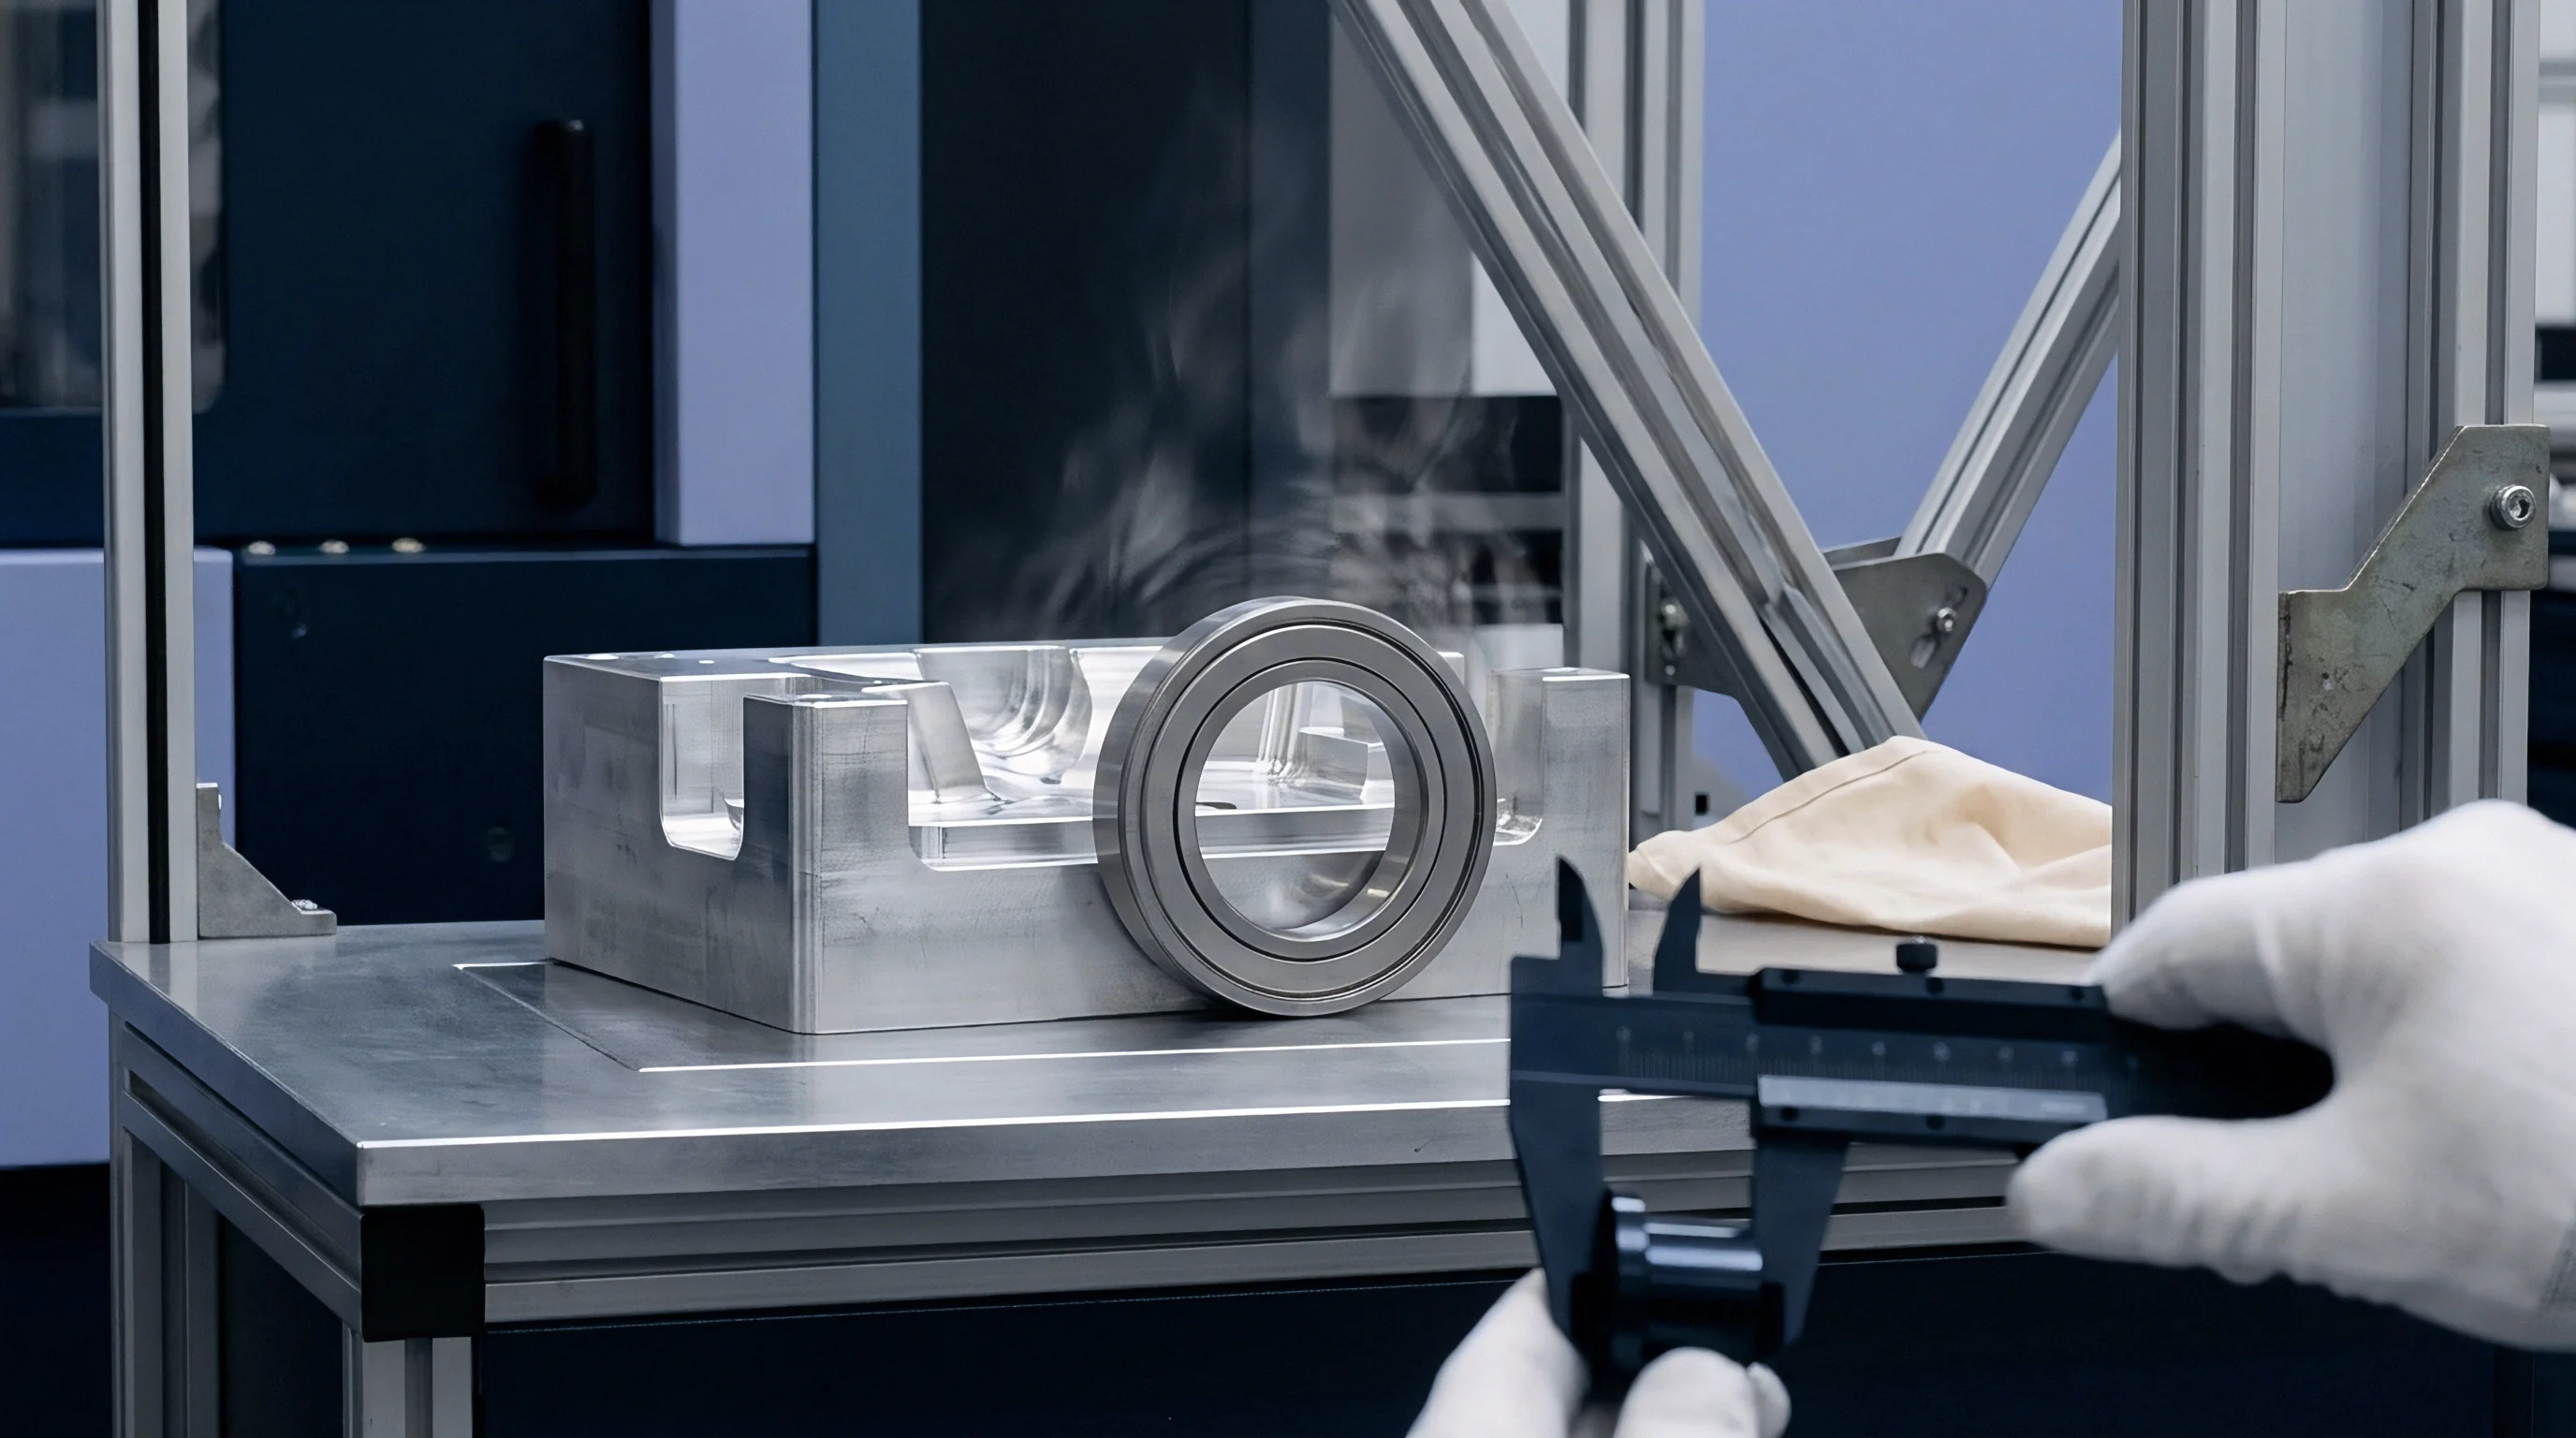
Incoming inspection protocols split verification into packaging integrity, physical mark comparison, and metallurgical assessment. The receiving team pulls three reels at random per inbound pallet. High-magnification optical inspection confirms pin-one orientation dimples, mold release impressions, and indentation depth against master golden component files.
Cloned microcontrollers and operational amplifiers routinely show chemical re-topping where acid dissolves original markings before laser etching applies high-spec part numbers. Blacktopping leaves distinct texture boundaries across epoxy packaging surfaces under sixty-times magnification, revealing microscopic swirl patterns that approved original component manufacturers do not produce.
Optical verification of lead frame plating thickness reveals unapproved base alloy substitutions before reels enter the surface mount placement lines.
X-ray fluorescence spectrometers positioned at goods inward verify lead-frame plating metallurgy in forty-five seconds per sample. Substituted passive components and semiconductor packages frequently substitute pure tin plating over brass for specified matte tin over nickel barrier layers. The lack of a nickel diffusion barrier precipitates tin whisker formation, creating latent short circuits across high-density board traces after forty to sixty operating days in the field.
When incoming parts fail composition limits, the stock system flags the entire lot code, locking inventory bins before replenishment dispatch requests clear.
Automated Bill of Materials Reconciliation
Enterprise systems track purchase orders, yet factory-floor kitting software often operates on unlinked local databases where line supervisors manually remap shortages to alternate suppliers. The discrepancy opens when production managers face line stoppage penalties and substitute functional equivalents without engineering change order approval. A factory line supervisor reassigns inventory numbers to meet the hourly output quota on a pick-and-place machine, bypassing the central enterprise database.
Bridging this gap requires daily reconciliation between real-time feeder setup sheets, automated surface-mount placement logs, and the contractually agreed bill of materials.
Modern pick-and-place systems read barcoded component carrier tapes as feeders load. Comparing machine setup logs against engineering revisions catches discrepancies before board loading begins. The verification software flags deviations where a reel scanned into slot twenty-two carries an approved resistance value but an unapproved brand or tolerance rating.
Discrepancies generate automated halts, locking the machine cycle until an authorized quality engineer enters a cryptographic release key tied directly to a signed engineering deviation notice.
The financial impact of line-level component swaps escalates across manufacturing stages. Catching a non-compliant capacitor at the receiving dock costs the component value and the handling labor. Finding that same capacitor after surface mount soldering multiplies the loss through manual rework stations, solder wick consumption, board de-lamination risks, and localized thermal stress from desoldering irons.
Catching the defect at end-of-line functional testing scraps finished assemblies, while field failure introduces freight callbacks, international warranty claims, and commercial litigation.
Dock
Golden Sample Microstructure Comparison
Destructive physical analysis operates as the primary defense against internal silicon substitution. Counterfeiters routinely house inferior small-die silicon inside standard footprint packages, potting the internal structure with excessive silica-filled epoxy. Decapsulation units utilizing fuming nitric acid at seventy degrees Celsius dissolve package resin within three minutes, exposing internal lead frames, bond wires, and die geometry.
Comparing internal die architectures under an optical metallurgical microscope directly against certified original golden samples exposes altered mask layouts, missing electrostatic discharge protection diodes, and non-approved manufacturer logos etched into the silicon substrate.
Bond wire material selection presents a massive commercial incentive for factory line substitution. Copper or silver wire alloys often replace specified ninety-nine point nine nine percent pure gold bond wires. This swap reduces raw component cost while introducing severe vulnerability to intermetallic corrosion at high ambient temperatures.
Scanning electron microscopy equipped with energy-dispersive X-ray spectroscopy measures the elemental signature of exposed bond wires, confirming purity levels and interface integrity at the ball bond weld.
| Component Category | Targeted Substitution Mode | Dock Inspection Method | Rejection Metric Threshold |
|---|---|---|---|
| Multilayer Ceramic Capacitors | Dielectric downgrading from X7R to Y5V | Thermal capacitance chamber sweep | Capacitance shift exceeding plus-minus fifteen percent at eighty-five degrees Celsius |
| Precision Resistors | Thin-film substituted with thick-film | Temperature coefficient test bench | Temperature coefficient drifting above fifty parts per million per Kelvin |
| Power MOSFETs | Die undersizing inside TO-220 cases | Nitric acid decapsulation and die measurement | Active die area reduction exceeding twenty percent of golden sample surface |
| Electrolytic Capacitors | Low-temperature electrolyte chemistry | Equivalent series resistance meter sweep | Impedance increase exceeding thirty percent above published nominal datasheet limit |
X-Ray Fluorescence Analysis of Contact Terminations
Contact pins and terminal leads represent standard targets for unauthorized alloy degradation. Connectors specified with gold flash over phosphor bronze often ship with cheap brass pins carrying flash plating thicknesses below zero point zero five micrometers. Handheld X-ray fluorescence guns deliver immediate quantitative measurement of surface metal thickness and base alloy composition.
The operator fires the instrument directly through the carrier tape blister, reading elemental spectra without compromising mechanical packaging.
The inspector matches the energy peaks for copper, zinc, nickel, and gold against nominal component qualification sheets. Inadequate nickel underplating permits copper atoms to migrate outward into the thin gold surface layer, oxidizing into non-conductive copper oxide films that disrupt low-voltage signal transmission. Detecting thin plating layers at the loading dock prevents field connector failures that manifest as intermittent bus communications weeks after deployment.
Production lots failing minimum gold plating thicknesses face immediate return to the sub-tier vendor at the vendor expense.
Warehouse staging spaces require isolated quarantine cages where flagged materials rest under physical padlocks. The dock receipt software denies warehouse placement transactions until chemical verification entries confirm specification compliance. Pallets holding unverified component reels carry distinct red placards detailing quarantine dates, part numbers, and testing lot IDs.
Material handlers face immediate disciplinary dismissal for moving quarantined inventory into active production bins without explicit clearance signatures from the plant quality director.
A supplier quality engineer notes that inventory shortages from certified distributors force purchasing agents to buy spot-market lots from Huaqiangbei brokers who provide fabricated certificates of conformance.
Furnace
Thermal Profiling and Solder Paste Rheology
Thermal reflow environments immediately expose clandestine component swaps that survive visual inspection. High-temperature plastics such as polyphenylene sulfide in terminal blocks and surface-mount connectors deform when factories quietly substitute cheaper polybutylene terephthalate formulations. Ten-zone reflow ovens operating lead-free SAC305 thermal profiles reach peak temperatures of two hundred and forty-five degrees Celsius.
Inferior polymers blister, warp, and dislodge internal contact pins under these thermal conditions, jamming pick-and-place lines and misaligning surface contact pads.
Substituted solder pastes present equal disruption to production integrity. Assembly facilities facing commercial margin pressure occasionally blend low-cost bismuth-bearing alloys into standard SAC305 solder paste pots, depressing the melting temperature to cut furnace electrical consumption. The introduction of unauthorized bismuth creates localized ternary tin-lead-bismuth alloys with brittle eutectic melting points near ninety-six degrees Celsius, destroying joint shock resistance.
In-line flux deposition sensors and solder paste inspection systems measure deposit volumes and height profiles at forty-micrometer resolution across printed circuit boards.
A contract line specifying pure silver paste deposits loses mechanical shear strength when unapproved bismuth additives alter the ternary alloy phase boundaries.
Real-Time Feeder Sensor Integration
Smart feeder technologies track component consumption rates and part weights directly on high-speed placement gantries. Modern motorized tape feeders integrate optical sensors that verify component thickness before the vacuum nozzle lifts the part from the embossed carrier tape. An unauthorized component substitution frequently presents a package height delta of zero point two millimeters compared to the original component drawing, triggering an instantaneous feeder abort signal that halts line indexing before defective placement occurs.
Automated optical inspection stations positioned immediately post-reflow examine component markings, terminal wetting fillets, and orientation polarity bands. Optical systems employ multi-angle colored LED lighting arrays to cast directional shadows across component edges. These reflections allow computer vision algorithms to detect mismatched component contours, missing manufacturer bevels, and wrong-color capacitor bodies characteristic of low-cost domestic component lines.
- Feeder load validation confirms that the optical barcode scanner matches the reel serial number against the engineering change order revision before the line motor energizes.
- Nozzle vacuum profiling checks component pick height and pneumatic seal pressure, aborting line cycles when part dimensions deviate from the programmed component library.
- Pre-reflow optical scanning checks part placement alignment and lead-to-pad coverage, marking boards with ink dots if package dimensions match unapproved vendor outlines.
- Solder joint meniscus tracking identifies insufficient wetting caused by non-compliant lead-frame oxidation or unapproved terminal finishes during reflow traversal.
- Automatic lane ejection diverts non-conforming boards onto offline diagnostic rails, alerting the resident quality engineer via terminal notifications.
Line supervisors frequently attempt to bypass feeder locks when production targets run behind schedule. Maintaining verification integrity demands that configuration parameters inside the surface-mount operating software stay locked behind administrative passwords held exclusively by the external client quality representative. When line managers lack the cryptographic authority to override feeder mismatch faults, production halts until the unapproved reel exits the feeder gantry.
Component substitution introduces catastrophic thermal stress variations during reflow soldering that permanently weaken circuit board laminates.
Circuit
In-Circuit Resistance and Inductance Fingerprinting
In-circuit testing rigs employ bed-of-nails fixtures that contact test points across assembled circuit boards within two seconds of placement. Flying probe systems deliver flexible alternatives for low-volume runs, moving micro-probes across test pads to measure individual passive and active component values in isolation. Unauthorized component substitutions stand out immediately under electrical parameter testing, as low-cost substitutes rarely replicate both direct-current resistance and high-frequency alternating-current impedance profiles simultaneously.
Ceramic capacitors substituted with inferior dielectric formulations reveal drastic voltage coefficients of capacitance under dynamic direct-current bias testing. An unapproved capacitor marked ten microfarads often drops to two microfarads when subjected to its rated twelve-volt operating potential, whereas the approved high-grade dielectric maintains eight point five microfarads under identical bias. Flying probe testers apply varying direct-current offset voltages during capacitance measurement sweeps, exposing unauthorized dielectric formulations that otherwise show correct values under zero-bias handheld digital multimeters.
| Parametric Variable | Specified Component Target | Substituted Clone Measurement | Test Condition Mechanics |
|---|---|---|---|
| Dielectric Absorption Rate | Below zero point one percent | Zero point eight to one point two percent | Fifteen-minute charge followed by one-minute open circuit recovery |
| Inductor Core Saturation Current | Four point five amperes at minus thirty percent | Two point eight amperes at minus thirty percent | Pulsed current sweep at one hundred kilohertz switching frequency |
| Leakage Current across Diodes | Maximum fifty nanoamperes | Six hundred to nine hundred nanoamperes | Rated reverse voltage applied at twenty-five degrees Celsius ambient |
| Resistor Shunt Thermal Drift | Twenty parts per million per Kelvin | One hundred and fifty parts per million per Kelvin | Current step loading driving component temperature to seventy degrees |
Boundary Scan and Silicon Stepping Interrogation
Counterfeit microcontrollers often match the pinout and basic execution instructions of specified parts while using older silicon steppings or stripped-down peripheral architectures. JTAG boundary scan architectures execute IEEE 1149.1 protocols to extract internal hardware identification registers directly through test access ports. Reading device identification codes, silicon stepping registers, and unique electronic chip serial numbers exposes factory substitutions where older, obsolete silicon or stripped factory-second chips sit on the assembly board.
Automated functional test benches run proprietary diagnostic firmware routines that interrogate internal memory block latencies and core voltage thresholds. Cloned microcontrollers fail register read-write cycle speed benchmarks when core execution clocks scale to specified operational maximums. Identifying altered processor identification numbers before packaging keeps boards out of final boxing stations, protecting downstream supply chains from intermittent field firmware crashes.
A typical board assembly running eight hundred components presents immense opportunities for unauthorized bill-of-materials margin shaving. Take an assembly run of fifty thousand units where a factory line manager substitutes five decoupling capacitors, a low-dropout linear regulator, and an operational amplifier with local uncertified clones. The unit savings per board appears modest at thirty-two cents across the substituted bill of materials.
Multiplied across the full run, the factory pockets sixteen thousand dollars in unapproved margin while shifting hundreds of thousands of dollars in long-term reliability risk to the brand owner.
Diagnostic firmware routines should mandate that internal cryptographic handshakes authenticate the silicon vendor root certificate before the bootloader authorizes peripheral power rails.
Ledger
Should-Cost Discrepancy Modeling
Material price divergence creates the commercial catalyst for unauthorized component substitution. Tracking raw market material pricing across public indices allows buyers to identify impossible factory quotes. When a contract manufacturer quotes an assembly price lower than the open-market procurement cost of the approved raw components plus energy and labor overheads, component substitution becomes an operational certainty.
Factories bridge this pricing deficit by acquiring factory overruns, reclaimed electronic parts from scrap recycling centers, and uncertified domestic alternatives.
Financial ledger surveillance compares component consumption against scrap reporting and purchasing records. In an operational production run of one hundred thousand printed circuit board assemblies, normal line setup and pick-and-place component drop rates consume between zero point three and zero point eight percent over nominal bill-of-materials requirements. If the factory material reconciliation reports zero reel drop losses while external invoices show identical purchases to nominal requirements, unrecorded reels entered the production line to compensate for dropped parts.
A component pricing variance exceeding twenty-two percent below authorized distributor contract tiers signals unauthorized spot-market inventory sourcing.
Sub-Tier Supplier Mapping and Invoicing
Transparency through second- and third-tier sub-suppliers stops unauthorized diversion. Contract manufacturers routinely issue purchase orders to authorized component distributors to secure documentation, cancel or divert those purchase orders before dispatch, and fulfill line staging using domestic grey-market inventory. Establishing direct commercial accounts with franchised distributors closes this avenue, requiring the factory to draw exclusively against dedicated client-owned inventory reserves.
Quarterly tripartite reconciliations between the brand owner, the contract manufacturer, and the franchised distributor verify that billed shipment quantities match completed board assemblies. Discrepancies between franchised distributor delivery manifests and factory production tallies expose unapproved sourcing channels before finished assemblies enter international transit lanes. The financial ledger provides clear empirical evidence of substitution long before physical parts demonstrate mechanical or electrical failure.
- Franchised distributor shipping logs cross-reference serial packing slips against inbound factory receiving tickets to prove component point of origin.
- Electronic data interchange reconciliation matches billing accounts payable records against production line yield scrap declarations every working week.
- Batch traceability certificates link wafer fabrication lot codes on reels directly to authorized original equipment manufacturer production schedules.
- Commercial payment escrow locks hold factory production margin disbursements until third-party material audits confirm all line reel lot codes match authorized procurement paths.
The distance between the brand engineering office and the factory production floor creates financial friction that bad actors exploit. A foreign enterprise managing assembly via periodic video calls and post-production quality reports remains structurally blind to sub-tier material swaps. Closing that distance requires physical line oversight, continuous raw material reconciliation, and hard contractual clauses that attach direct commercial penalties to unapproved material swaps.
What specific test method proves that passive components inside potted automotive subassemblies meet specification without destroying the outer mechanical housing?
Remedy
Contractual Allocation of Substitution Liabilities
Commercial contracts govern factory behavior when line incentives favor unapproved substitutions. Standard manufacturing agreements frequently dilute buyer protections through vague quality clauses that lack specific operational definitions for component tampering. A manufacturing contract must define an unauthorized component swap as a non-curable material breach of contract that triggers immediate liquidated damages rather than standard rework cycles.
The contract language must explicitly eliminate the defense of commercial equivalence, stating that any unapproved component swap invalidates factory compensation claims for the entire manufacturing batch.
Liquidated damages clauses set financial penalties that exceed the commercial gain of the component substitution. If a factory saves ten thousand dollars by substituting unapproved surface-mount transistors, standard damages merely seeking replacement costs create zero deterrent. Contract terms must stipulate that discovering an unauthorized component substitution triggers an immediate assessment of three times the total production run value, alongside full commercial reimbursement for third-party forensic disassembly, metallurgical testing, and global logistics recall expenses.
Escalation Protocols and Production Holds
Operational escalation begins the moment dock inspections or line sensors register a part mismatch. The resident quality representative executes an immediate stop-ship notice on the entire lot, notifying international logistics forwarders to hold container dispatches at port terminals. The factory management receives a formal non-conformance report requiring complete material quarantine within two hours of discovery, backed by the physical presence of the buyer local representative on the factory floor.
Resuming production requires executing a structured five-point validation protocol before machinery re-energizes. The supplier purges all component bins, feeders, and intermediate warehouse buffers, returning unapproved lots to external distributors under documented supervision. Authorized franchised distributor components restock the feeder tracks, followed by destructive cross-section testing of twenty initial production boards across all active surface-mount lines.
The factory covers all testing fees, scrap expenses, and line downtime overheads, embedding the real operational cost of component substitution directly into the supplier monthly financial ledger.
Section 14.2 of the International Manufacturing Master Services Agreement specifies that the discovery of any unapproved component substitution across active production reels empowers the buyer to seize all factory-held tooling and production jigs without judicial intervention while offsetting forensic inspection expenses against pending finished goods invoices.