Meaning
Administrative protocol regulates the sequence of material transfers between processing stations during continuous production runs. Operators utilize reel change queuing to coordinate the depletion of one supply roll with the engagement of a fresh substrate, ensuring that mechanical tension remains constant across the interface. This synchronization prevents stoppage by aligning the physical exhaustion of active material with the entry of the successor.
Authorities such as the General Administration of Customs recognize this control methodology as a critical audit point for manufacturing throughput verification.
Operational Sequence
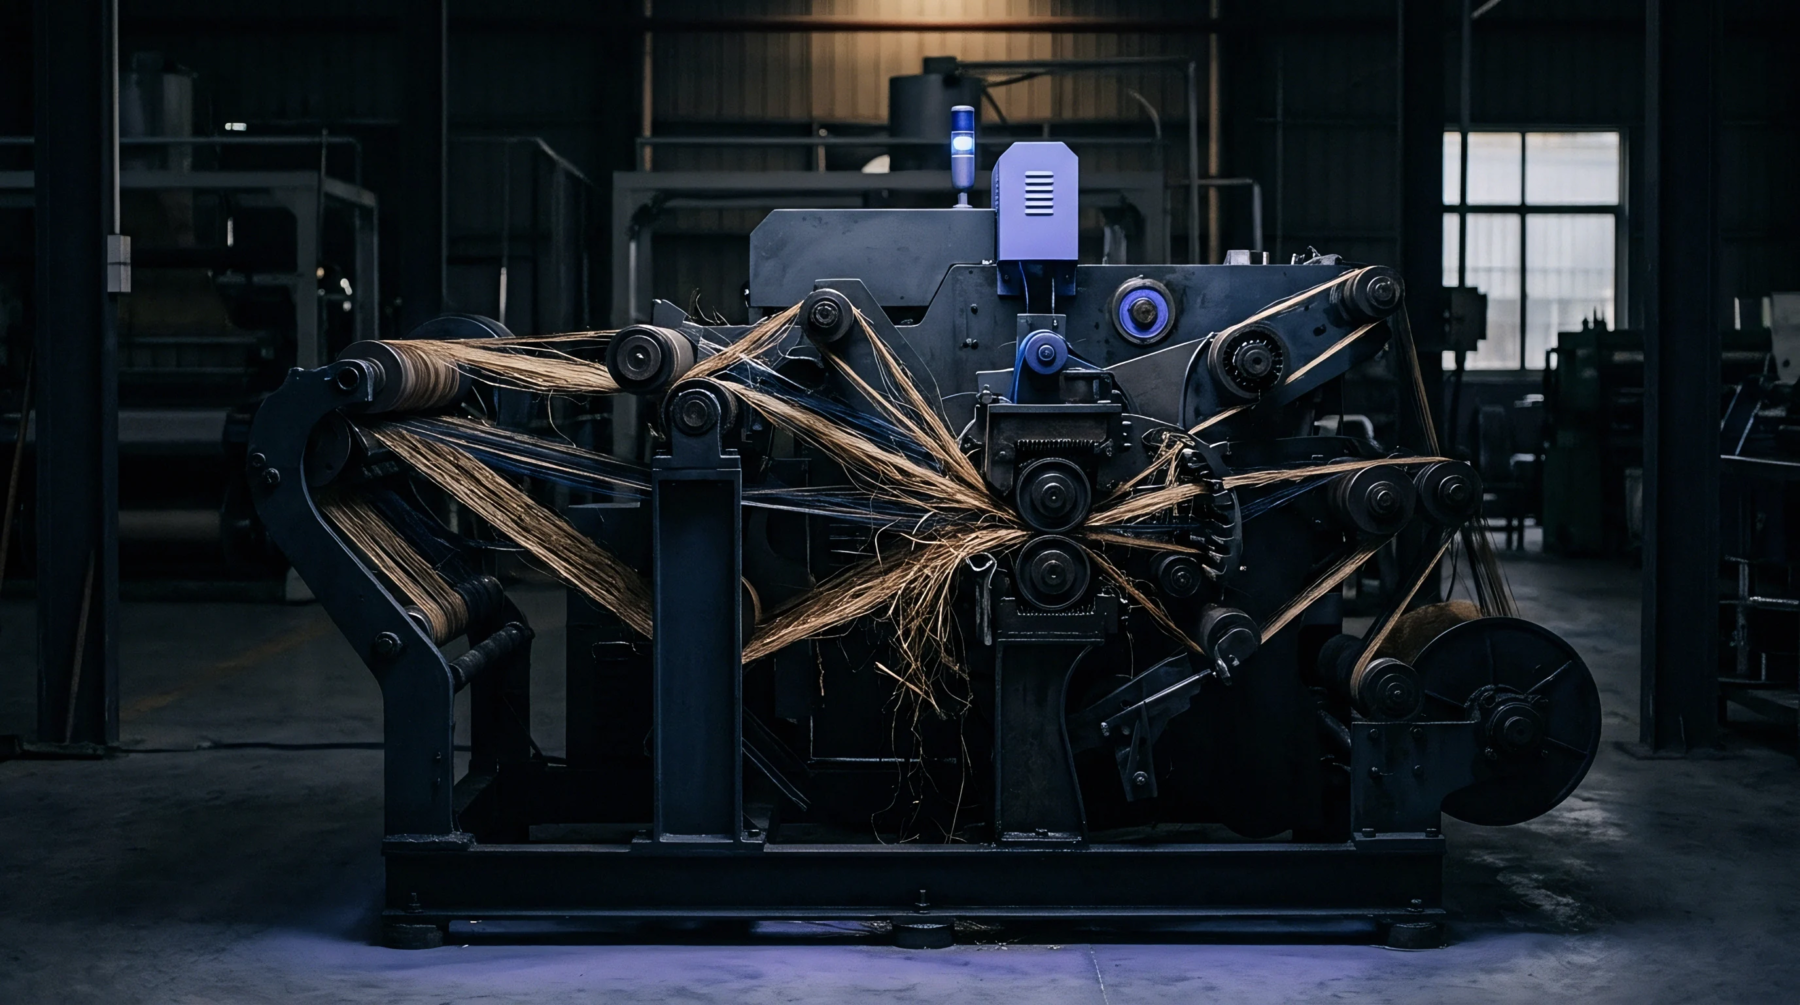
Machine configurations rely on this method to sustain high speed output without manual intervention between units. Controllers monitor diameter sensors on the active mandrel to trigger a logic signal when the material reaches a threshold diameter. Precise mechanical arms then position the replacement spool for an instantaneous splice or transfer.
Systems manage the interface velocity so that the surface speed of the incoming roll matches the outgoing web before contact occurs. Deviations in this automated timing lead to web breaks or irregular tension profiles that damage the structural integrity of the final goods.
Jurisdictional Requirement
Chinese commercial regulations require documentation of these process parameters during factory inspections to validate production capacity claims. Factories maintain records of splice success rates and dwell times as part of their environmental and quality management filings. Authorities examine whether the equipment operates within the parameters declared in the original import filing for the manufacturing machinery.
Compliance depends on the ability of the plant to demonstrate that the actual production cycle matches the registered automated performance profile. Any discrepancy during a surprise audit risks the reclassification of duty exemptions previously granted for high efficiency equipment imports.
Audit Mechanism
Verification involves reviewing the log files stored within the programmable logic controllers attached to the processing line. Auditors extract timestamped data showing the interval between the queuing trigger and the execution of the material swap. Discrepancies between the intended sequence and the recorded data indicate mechanical wear or software modifications that fall outside the authorized technical specifications.
Stable performance across these transfer points proves that the machinery functions according to the technical standards filed during initial regulatory approval. Proper management of this sequence remains the primary indicator of operational consistency for complex production lines.