Meaning
Material properties inherent in the body centered tetragonal crystal structure of pure tin determine the non-uniform physical responses of the metal when subjected to varying directions of external force or temperature change. In the field of semiconductor packaging beta tin anisotropy describes how electrical and mechanical coefficients vary significantly along different axes of the grain structure. This term governs the predictable variation in thermal expansion and modulus values within solder joints of microelectronic devices.
It stops applying when the tin reaches its melting point and shifts into a liquid state or when it transforms into alpha tin at low temperatures. In high volume electronics manufacturing the orientation of the tin grains dictates the long term survival of a connection under cyclic thermal loading.
Crystal Orientation
Microscopic arrangements of the atomic lattice create distinct directions for heat flow and stress dissipation within a single grain of the metal. Because of beta tin anisotropy the coefficient of thermal expansion along the long axis of the crystal is nearly double the value found along the short axis. This discrepancy generates internal localized stresses when the solder joint cools after the reflow oven cycle or heats up during device operation.
Large grains that span the entire width of a bump create a single unified direction of expansion which often results in premature failure. Fine grained structures minimize this effect by averaging the expansion directions across many randomly oriented small crystals. Controlling the cooling rate of the board determines which grain pattern dominates the final solidified structure of the bump.
Mechanical Stress
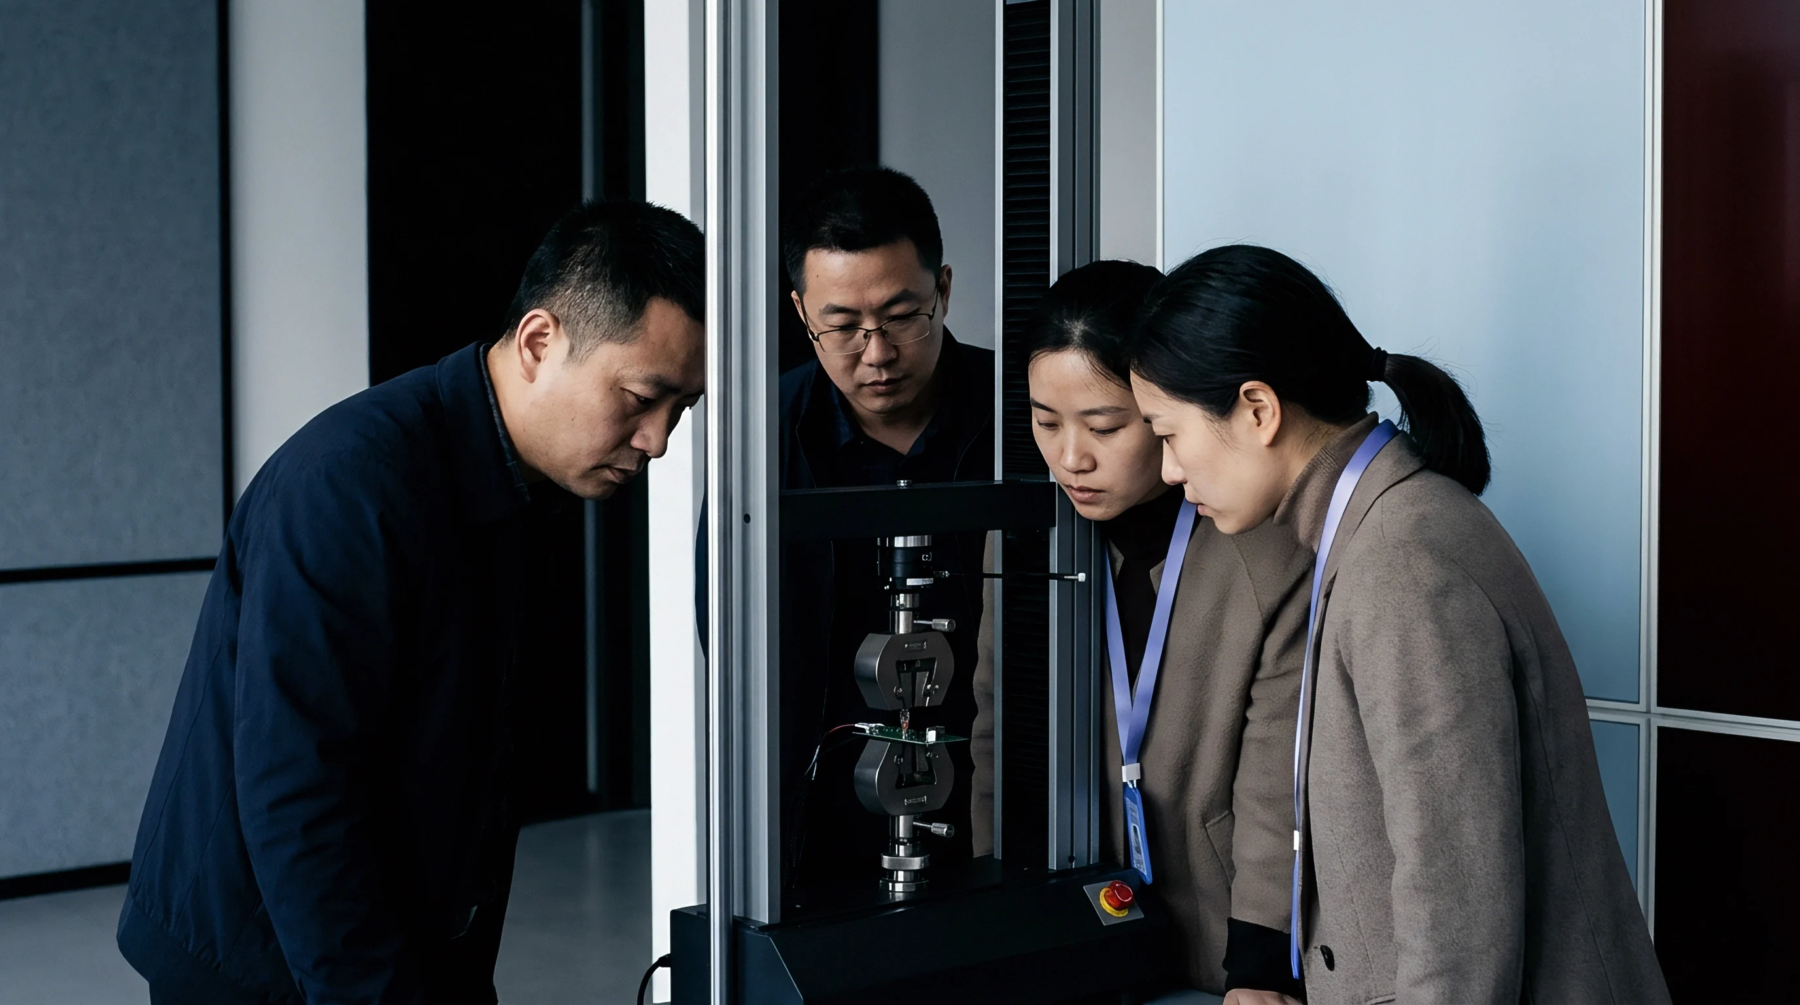
Deformation behaviors under mechanical load show high sensitivity to the angle of the applied shear relative to the grain boundary. Within the study of beta tin anisotropy investigators find that stiffness levels change as the internal geometry of the crystal rotates during stress events. Solders undergo creep differently based on the orientation of these tetragonal blocks which leads to uneven thinning of the joint during long term deployment.
This property makes predicting the exact time to failure difficult without high resolution orientation imaging microscopy of the sample. Stiff grains transfer more energy directly to the fragile silicon layers above the joint which increases the risk of cratering or interfacial delamination. Interfacial chemistry between the tin and the copper pad interacts with this anisotropy to define the toughness of the intermetallic layer.
Reliability Impact
Failure modes in consumer devices frequently trace back to the cumulative effects of these directional properties during power cycling. Through the lens of beta tin anisotropy modern engineers explain the sudden formation of tin whiskers and the rapid propagation of fatigue cracks. Cracks tend to follow paths that minimize the resistance offered by specific crystal planes within the bulk material.
Mitigating these risks requires adding trace elements like silver or copper to the alloy to encourage grain refinement and decrease single crystal dominance. Tests involving thousands of thermal cycles confirm that joints with random grain orientations last longer than those with oriented column structures. This material behavior serves as the primary constraint in the design of next generation high density chip arrays using lead free materials.
Logic dictates that smaller bumps face higher relative risks from single grain dominance.