Contractual Execution Mechanics and Operational Oversight Strategies for Micro Batch Hardware Manufacturing
Micro batch hardware procurement requires milestone tranche payments, explicit scrap deduction formulas, and physical line oversight to prevent cost overruns.


Gauge
Micro batch hardware production creates immediate tension between fixed tooling costs and component variance. When an engineering team orders five hundred units of a specialized IoT hub or medical monitoring enclosure, the supplier treats the job as a gap-filler between high-volume runs. Factory engineers allocate minimal setup time, assign secondary assembly lines, and rely on off-the-shelf fasteners or enclosures to protect their margins.
Distance only adds to unit overhead. As a result, failure points shift away from automated high-speed assembly toward manual alignment, erratic torque application, and sub-tier component substitutions.
Contractual agreements for low-volume production must account for these operational realities through explicit engineering specifications, defined tolerance stacks, and clear Non-Recurring Engineering (NRE) terms. Standard master service agreements designed for tens of thousands of units fall apart in micro batch environments. They offer no real remedies for extended setup times, partial component staging, or high initial scrap rates while balancing the line.
Drafting a proper micro batch agreement means embedding precise dimensional thresholds, inspection frequencies, and tooling transition mechanics straight into the primary contract schedules.

Engineering Drawing Sign off in Low Volume Runs
Dimensional tolerances set during rapid prototyping rarely translate directly to short-run manufacturing lines. Prototypes usually rely on additive manufacturing or high-precision computer numerical control (CNC) machining. Small-batch factory production, by contrast, frequently shifts those same parts to soft-tool injection molding or low-cost aluminum casting to trim upfront tooling expenses.
An initial enclosure prototype specified a 15-micron tolerance on the mounting pins, only for the short-run supplier to use casting molds that held merely 50 microns under standard thermal conditions. The resulting variance caused assembly interference, forcing factory operators to ream plastic holes manually during final assembly.
To stop unmonitored floor modifications before they start, the contract enforces a formal Engineering Drawing Sign-Off protocol prior to initial line setup. Sign-offs bind both parties to specific geometric dimensioning and tolerancing (GD&T) standards under ASME Y14.5-2018. The contract stipulates that any variance beyond drawing callouts constitutes a non-conformance, whether or not the assembled unit works during functional testing.
Low-volume buyers have to define nominal dimensions alongside lower and upper specification limits for critical interfaces, PCB mounting hole patterns, external port alignments, and thermal interface contacts.
Off-the-shelf components brought in to cut BOM costs introduce their own dimensional drift. Passive electronic components, connectors, and generic plastic housings sourced from open domestic markets carry looser tolerance bands than custom-molded parts. Contracts must state that commercial off-the-shelf (COTS) variations remain the factory’s financial responsibility if the factory handles procurement.
When the buyer supplies COTS parts instead, the agreement establishes receiving inspection criteria (AQL 1.0 General Inspection Level II per ISO 2859-1) to validate dimensions before components ever reach the assembly floor.

Contractual Allocation of Non Recurring Engineering Costs
Tooling and setup charges take up a disproportionate share of the budget in runs under two thousand units. Suppliers frequently quote deceptively low unit piece prices while inflating NRE line items to protect their margins on short runs. Contract execution mechanics need to separate NRE costs into distinct categories: physical mold development, custom test fixture fabrication, SMT stencil creation, and line conversion labor.
Each category must carry specific acceptance criteria before escrow funds are released or invoices get approved.
Soft tooling like aluminum injection molds or silicone vacuum casting setups wears down fast. An aluminum mold rated for two thousand shots starts losing dimensional stability by fifteen hundred cycles from thermal degradation and parting-line wear. The contract must declare the expected lifespan of soft tooling and fix explicit responsibility for refurbishing or re-cutting tools when dimensions drift out of spec.
Buyers retain full ownership of all custom tooling, stencils, jigs, and firmware flashing devices, regardless of where NRE funding comes from or how payments are amortized into unit costs.
| Contract Mechanism | Standard Volume Provision | Micro-Batch Adapted Provision | Operational Risk Mitigated |
|---|---|---|---|
| NRE Cost Allocation | Amortized across 100k+ units in unit piece price | Milestone payments tied to First Article Inspection (FAI) approval | Supplier abandonment after initial setup cash absorption |
| Defect Acceptance (AQL) | AQL 0.65 Major / 1.5 Minor (ISO 2859-1) | Zero-defect acceptance on critical safety features; AQL 1.0 Major | Statistical sampling passing defective low-volume batches |
| Tooling Ownership | Supplier holds tooling until production end-of-life | Immediate title transfer upon setup payment; factory storage fee fixed | Hostage tooling during commercial payment or scrap disputes |
| Line Setup Scrap Allowance | 1% to 2% absorbed by supplier | Tiered scrap allowance: 5% first 100 units, 1% on remaining run | Supplier inflating unit price to cover setup yield loss |
Setup costs for Surface Mount Technology (SMT) pick-and-place lines are another constant source of friction. A short run of two hundred circuit boards still requires feeder loading, solder paste printing setup, reflow profile validation, and optical inspection programming ~ tasks that demand the exact same labor hours as a ten-thousand-unit run. Suppliers often try to absorb setup costs into unit pricing upfront, only to demand higher volumes mid-production.
The contract needs to isolate SMT setup charges into flat-fee line items triggered strictly upon physical setup completion. Clear pricing schedules prevent mid-run fee renegotiations when order sizes shift.
Clause 14.2 of the Master Electronics Supply Agreement converts standard defect penalties into immediate credit memos against active component inventory whenever yield falls below ninety-four percent.


Jig
Small production runs on the factory floor rely on physical hold-downs and alignment brackets to minimize operator error. High-volume operations can justify automated, sensor-monitored pneumatic fixtures that guarantee precise mechanical positioning. Micro batch runs, on the other hand, lean heavily on manual assembly fixtures, cheap acrylic plates, and hand-clamped guides.
These inexpensive fixtures wear down fast, lose alignment, and accumulate assembly errors over a fifty-unit shift. Physical verification of temporary alignment aids is therefore essential to micro batch oversight.
Responsibility for fixture design and verification sits squarely between the client’s engineering team and factory floor supervisors. When a buyer submits 3D CAD models, the factory builds basic holding tools to assist assembly. The contract must mandate that these production aids undergo dimensional verification against golden samples before the primary production run starts.
Without explicit contractual controls, factories will run short batches using uncalibrated hand tools, leaving the buyer with skewed board seating, pinched wiring harnesses, and erratic torque on structural screws.
Tooling Ownership and Maintenance Mechanics
Physical possession of production jigs, SMT stencils, and test fixtures gives suppliers huge leverage during commercial disputes. Contract terms must explicitly state that all custom fixtures built for a specific run remain the sole physical property of the buyer. The contract should mandate permanent engraved tags on every fixture, identifying the buyer’s name, part number, and serial code.
Between short production runs, suppliers must store these items in climate-controlled spaces to prevent corrosion and warping.
Fixture wear directly degrades dimensions in molded plastic and stamped metal components. Soft aluminum molds and manual clamping jigs drift out of spec after remarkably few cycles. A dedicated contract clause should require the factory to maintain a physical usage log attached to each fixture, tracking clamping cycles, maintenance dates, and repair history.
Once a fixture reaches eighty percent of its rated cycle life, the supplier must notify the buyer to arrange for re-machining or replacement under agreed financial terms.
Because tooling wear alters dimensions, the contract must establish a strict First Article Inspection (FAI) process for every new micro batch run ~ even if the product was manufactured on that exact line before. Line teardowns and re-setups introduce alignment variables that render past inspection passes completely irrelevant to the current run.
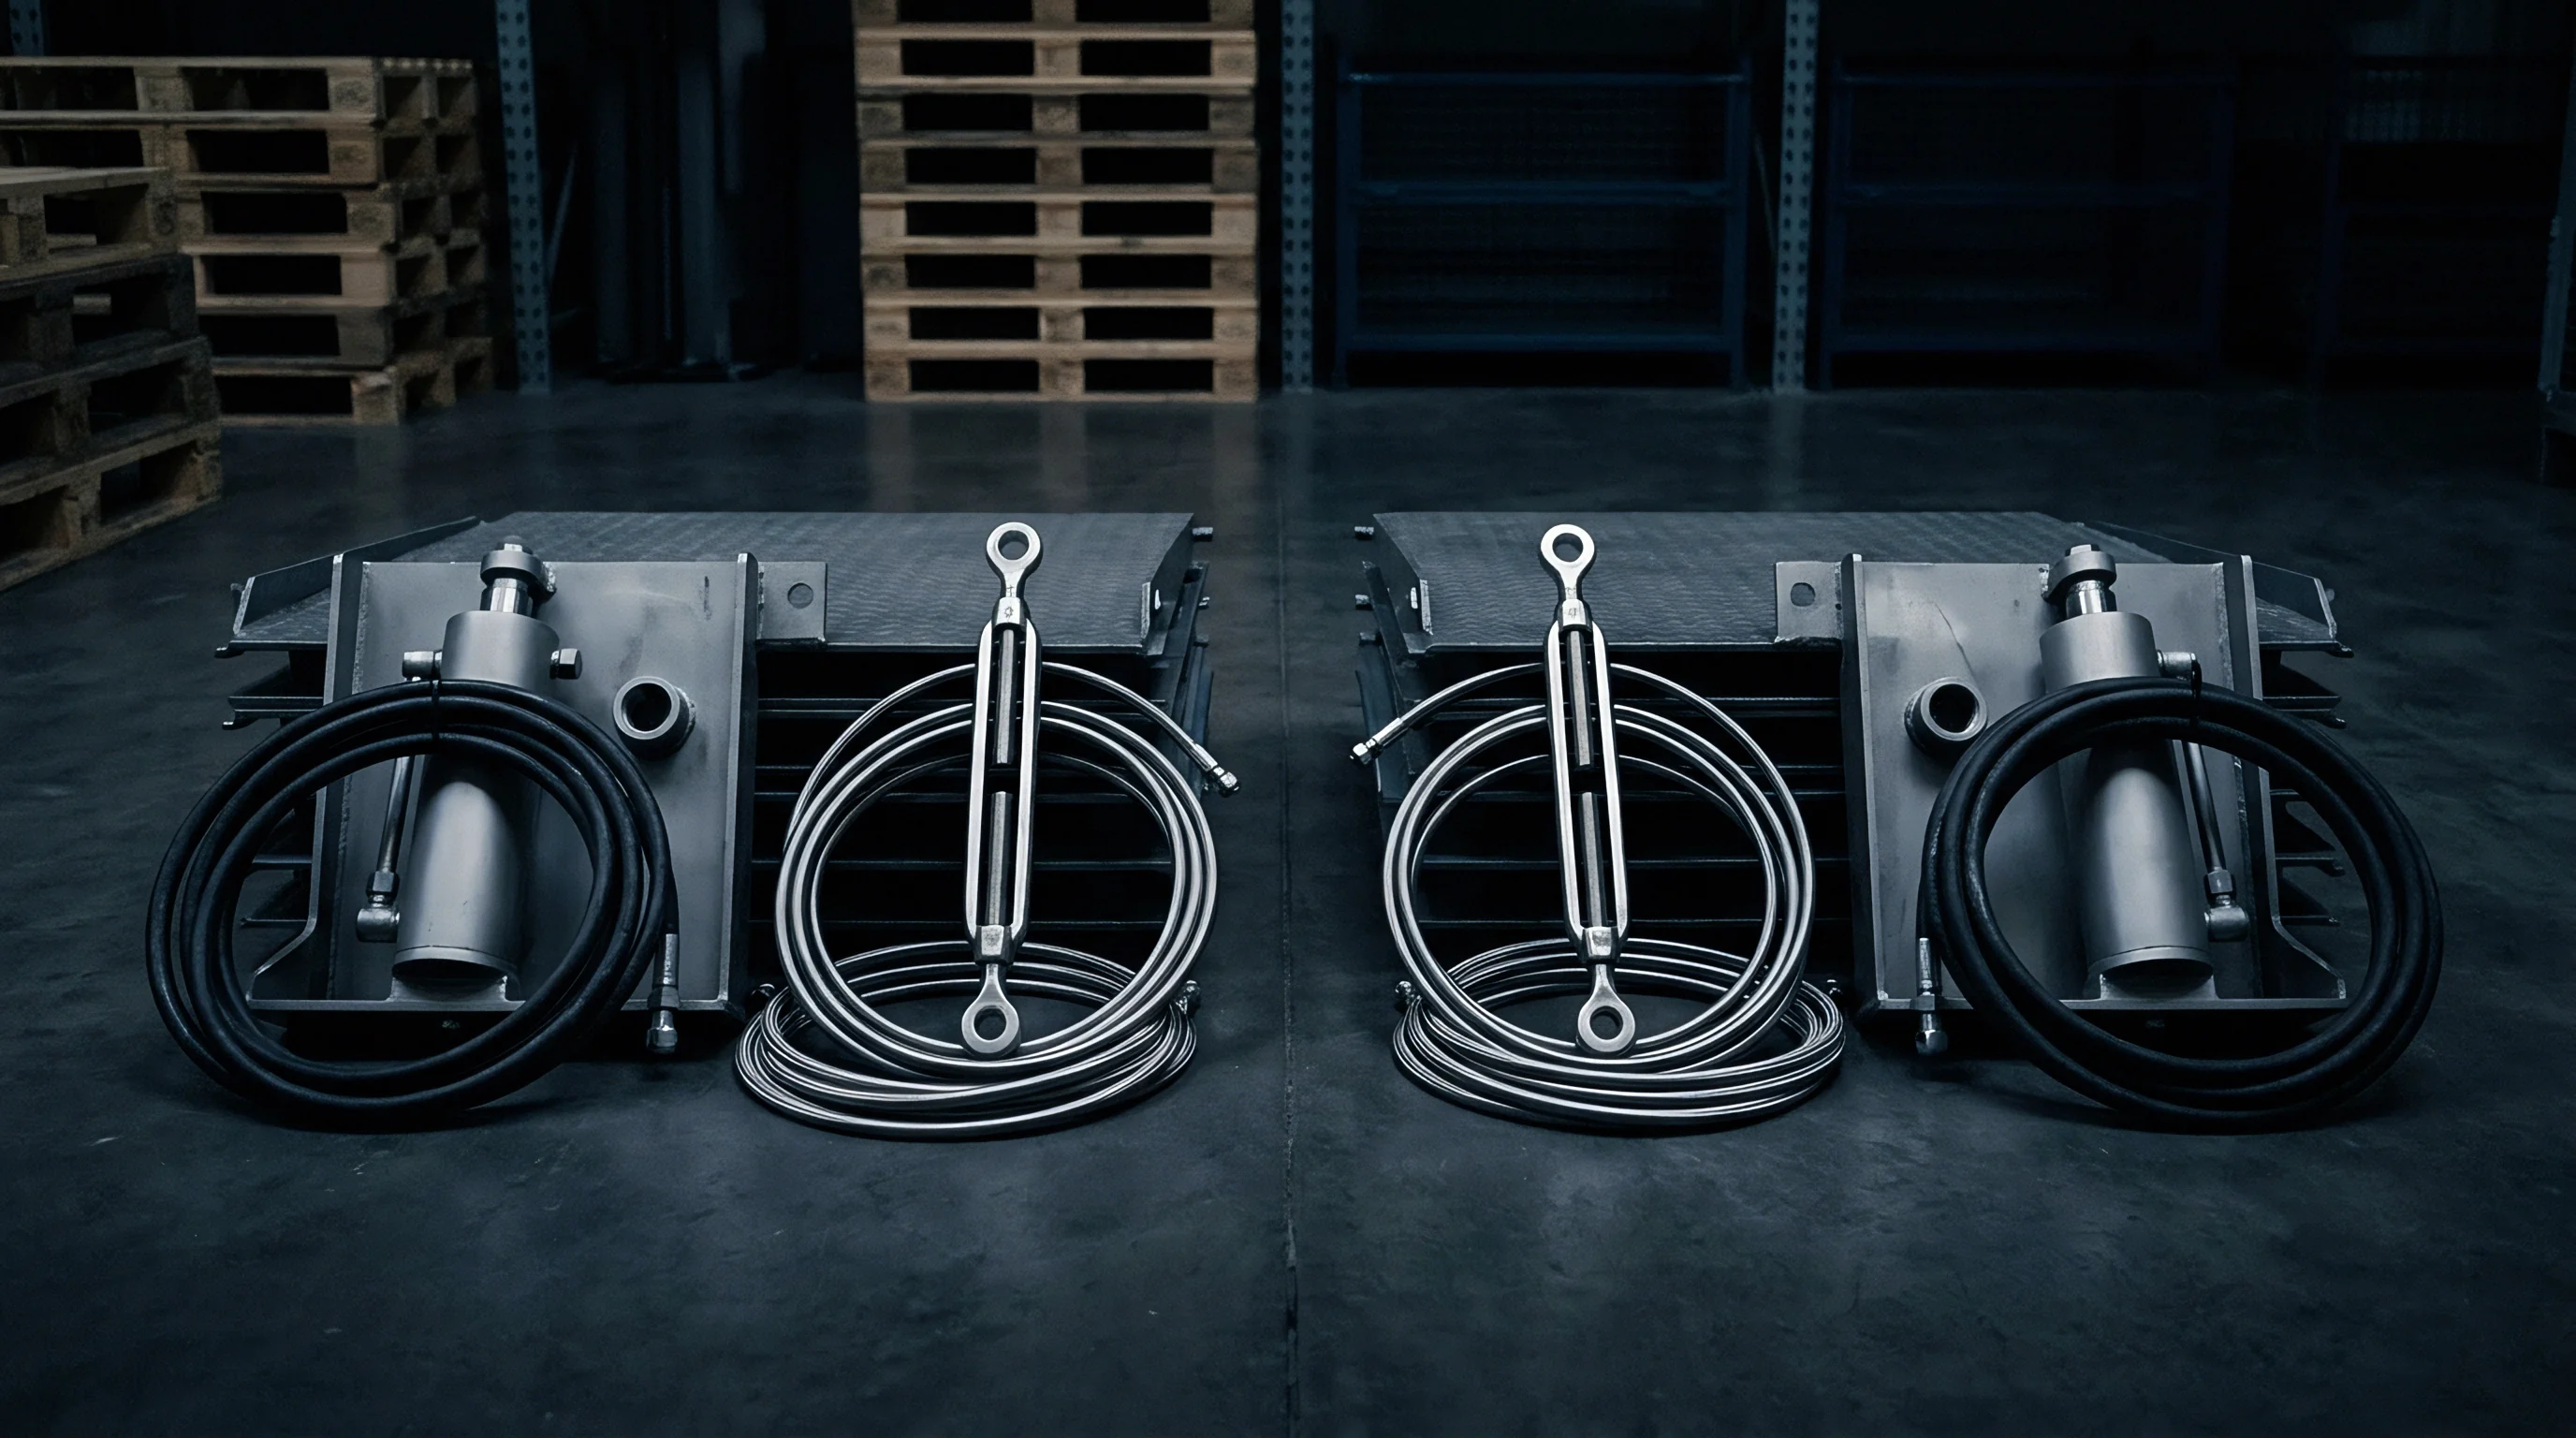
Whose Line Calibration Controls First Article Approval?
Line calibration means matching physical assembly jigs, torque screwdrivers, reflow ovens, and automated test stations to the exact technical requirements of the engineering build package. Disputes often arise when the factory claims its standard line setup is fine, while the buyer insists on custom calibration routines. The contract must stipulate that the buyer’s written First Article Inspection checklist governs line approval.
The factory cannot start mass assembly until an authorized buyer representative or designated third-party auditor signs off on the FAI certificate.
First articles set the baseline. Line operators build five to ten units under direct observation during FAI, and engineers measure those units against every drawing dimension, weight limit, electrical requirement, and aesthetic standard. If even one unit fails dimensional checks because of misaligned fixtures, the line stops immediately.
The factory has to adjust the jig, re-verify physical offsets, and produce a fresh five-unit FAI sample. Any labor costs from calibration delays stay entirely with the supplier if the delay stems from factory-provided tooling failures.
- Uncalibrated Manual Clamps lead to variable board insertion depths, putting stress on internal connectors and causing intermittent power loss during transit vibration.
- Worn SMT Stencils cause solder paste bridging across fine-pitch QFN pads, driving up short-circuit rates on initial board power-up.
- Acrylic Routing Guides deform or melt under heat gun exposure during manual cable jacketing, leaving scratches across the exterior housing.
- Unmatched Torque Drivers strip plastic mounting bosses or leave structural screws loose, leading to failures in mechanical drop tests during final packing.
- Generic Pogo Pin Plates miss critical test points on dense PCBs, allowing unprogrammed or partially flashed microcontrollers through assembly.
The contract should also enforce strict controls over tools at manual rework stations. Small-batch factories frequently use uncalibrated soldering irons, unregulated hot air guns, and generic liquid flux during component touch-ups. These unvetted tools introduce thermal stress, board delamination, and corrosive residue.
Contract schedules ought to list approved hand tools, operational temperature ranges, and no-clean flux specifications so manual touch-ups don’t degrade product lifespan.
Line switchovers under twenty-four hours force the shop floor to run uncalibrated manual press fixtures or delay production by three full calendar days.
Cadence
Short manufacturing runs compress review windows from months into hours. A run of one thousand units can finish in under forty-eight hours once components hit the floor. Standard monthly or bi-weekly status calls are completely useless here ~ by the time a bi-weekly call comes around, the entire batch might already be assembled, packaged, and loaded into a shipping container with systematic assembly defects baked in.
Managing short production bursts takes real-time floor communication, daily shift reviews, and fast escalation paths.
Oversight cadence has to match the physical pace of the floor. That means building communication loops synchronized directly with factory shift schedules. When operating across major time zone gaps, drop long email chains in favor of structured digital updates, real-time messaging shift logs, and mandatory floor photos taken at clear assembly milestones.
Managing at a distance requires relentless schedule discipline.

Daily Shop Floor Reporting Rhythms
Daily reporting during a micro batch run needs detailed operational data, not vague status updates. An acceptable shift report contains exact figures for component intake, units through SMT, units through final assembly, units passing functional testing, and scrap counts categorized by failure mode. If yield drops without explanation from ninety-eight percent to ninety-one percent between shifts, operational managers need to investigate immediately before the line starts up again the next morning.
Active assembly demands three daily communication checkpoints. First, a pre-shift briefing confirms that component staging is complete, operators are trained on the latest work instructions, and test stations are working. Second, a mid-shift check delivers raw throughput numbers and initial defect rates.
Third, an end-of-shift report details final counts, scrap logs, and photos of quarantined non-conforming units. This rhythm keeps short production runs entirely transparent.
ISO 9001 Clause 8.5.1 mandates that organizations control production and service provision under specified conditions, including the availability of documented information defining product characteristics and monitoring activities.
When discrepancies pop up during shift reviews, the contract must enforce an immediate halt-of-production rule. If defect rates cross an agreed threshold ~ say, three percent of shift volume ~ the line stops automatically. Assembly cannot resume until factory quality leads and buyer engineers finish a root-cause analysis and sign off on a corrective action plan.
Engineering Change Order Execution during Live Production
Micro batch runs often coincide with active hardware development, making mid-production changes inevitable. An engineering team might uncover a firmware issue that calls for a different hardware component, or a physical gap that requires an extra insulating spacer inside the case. But pushing an Engineering Change Order (ECO) during a short run carries real operational risk.
A mismanaged ECO leads to mixed-revision inventory, scrapped components, and arguments over downtime costs.
Contractual ECO protocols must lay out explicit steps for modifying live production lines. Any change requires written acknowledgment from the factory general manager before taking effect ~ phone calls or quick chat messages do not authorize engineering updates. The ECO document must specify the exact serial number range where the change takes effect, what happens to older components (scrap, return, or rework), and any adjustments to unit pricing or setup fees.
| Production Event | Trigger Condition | Mandatory Escalation Action | Contractual Timeframe |
|---|---|---|---|
| First Article Failure | Single dimensional or functional failure during initial 5 units | Halt assembly; re-align fixtures; perform secondary FAI pass | Immediate notification; 2-hour resolution window |
| Shift Yield Drop | Yield falls below 95% across any 4-hour monitoring block | Stop line; audit SMT reflow profile or manual operator steps | 4-hour notification window; written shift log required |
| Unscheduled Changeover | Factory attempts line switch due to missing internal parts | Hold components in secured cage; audit remaining inventory | 12-hour written notice required prior to line movement |
| Component Variance | COTS part dimension or lead spacing differs from spec sheet | Isolate batch; run test sample; obtain buyer waiver | 24-hour engineering disposition deadline |
Handling mixed revisions within a short run requires clear visual and physical segregation. The factory must apply distinct revision stickers to assembled circuit boards, internal housings, and exterior packaging boxes. Unmodified components must be physically pulled off the line and returned to secure staging cages before modified parts hit the stations.
Failing to enforce line clearance during an ECO almost always results in mixed revisions shipping under the same serial numbers.
A silent afternoon on the factory floor usually means component shortfalls or unannounced manual rework.


Freight
Component logistics in micro batch hardware builds represent a major vulnerability for both schedules and budgets. High-volume programs run steady component pipelines backed by warehouse buffer stock. Micro batch builds, by contrast, rely on just-in-time delivery of small quantities across fragmented supply chains.
One missing microcontroller, custom gasket, or specialized connector halts the entire run. Component staging, material receiving audits, and customs strategy must be written directly into the contract.
Logistical control hinges on managing the Bill of Materials (BOM) staging timeline. Contract terms should enforce a full BOM Staging Audit ten business days before the scheduled assembly date. Production must not be scheduled until one hundred percent of active components sit inside the factory warehouse and have passed receiving inspection.
Starting production with a ninety-five percent complete BOM leaves partial builds sitting unsealed on the floor, exposed to moisture, dust, and handling damage while everyone waits on missing parts.

Kitting Audits and Material Staging Protocols
Material kitting turns bulk component inventory into sub-assembly packages assigned to specific workstations. In small-batch production, that kitting process needs direct verification before any parts move to the floor. Warehouse staff must check part numbers, manufacturer lot codes, reel packaging, and moisture sensitivity levels (MSL) across all integrated circuits.
Moisture-sensitive components require explicit baking protocols if vacuum seals were broken during transit or inspection.
The pre-shipment component staging procedure enforces strict material readiness controls before assembly labor begins:
- Count and cross-reference all received component line items against the master engineering Bill of Materials using physical reel and box counts.
- Inspect vacuum sealing indicators and humidity indicator cards on all moisture-sensitive surface-mount ICs prior to SMT reel loading.
- Perform dimensional and electrical parametric checks on five sample units per component lot using calibrated meters and optical comparators.
- Verify that custom molded parts, stamped metal shields, and printed circuit boards carry correct revision stampings matching current drawing files.
- Package fully verified component sets into physical kit bins designated by assembly line station, securing bins within a locked material holding cage.
Factory-sourced off-the-shelf components introduce grey-market and counterfeit risks to micro batch builds. Suppliers up against tight lead times frequently buy passives or microcontrollers from independent brokers instead of authorized distributors. To limit this exposure, the contract must require full Certificates of Conformance (CoC) and chain-of-custody documentation for every item on the BOM.
If broker sourcing is unavoidable because of market shortages, the factory must run functional and structural authenticity tests at an accredited third-party lab before those parts ever touch an assembly kit.
Air freight expedited fees for late-arriving SMT components increase overall logistics overhead by up to thirty-two percent per unit on runs under one thousand items.
Delays compound fast. Component stockouts mean idle line charges billed by the factory if the buyer supplied the parts, or schedule breach penalties billed to the factory if they managed procurement. Contract terms need flat, predictable rates for idle line downtime, along with clear cutoff thresholds for when a delayed run must be rescheduled without penalty.

Customs Valuation and Partial Shipment Splits
Shipping finished micro batch goods internationally introduces legal and commercial friction over customs valuation, tariff classification, and paperwork. Low-volume runs usually ship via express couriers (FedEx, DHL, UPS) rather than ocean containers. Express customs clearance relies heavily on flawless commercial invoice declarations ~ inaccurate tariff codes or understated component values lead directly to customs holds, surprise duty assessments, or seized cargo.
When yields drop below target, factories frequently suggest partial shipments to meet original delivery deadlines. If a run of one thousand units yields only six hundred passing units on the ship date, the factory sends the six hundred and holds four hundred for rework. The contract needs explicit rules governing how freight, customs entry fees, and documentation costs are split on partial shipments.
If the yield shortfall was caused by factory quality failures, the supplier should pay all air freight and handling fees for the follow-up delivery.
Customs valuation rules require declaring the full transaction value of goods, including amortized tooling and engineering setup costs if billed separately. If a buyer pays fifty thousand dollars in separate NRE setup fees and orders five hundred units at ten dollars a piece, customs authorities may assess duty against the combined value of one hundred ten dollars per unit rather than the unit invoice price alone. Contracts should specify which party bears liability for duty adjustments stemming from non-amortized engineering fee structures.
The unresolved commercial question remains whether buyers can legally bind sub-tier component distributors to air freight liability when raw material lead times slip past agreed windows.

Settlement
Financial settlement terms dictate how a factory actually behaves on the floor. Micro batch agreements require payment structures that align the factory’s incentives with the buyer’s quality expectations. Standard high-volume terms ~ like thirty percent deposit with seventy percent balance due on bill of lading ~ leave buyers exposed on small runs.
Once a factory holds eighty or ninety percent of total contract value, its motivation to resolve trailing quality issues or perform tedious rework on small batches drops off a cliff.
An effective micro batch structure splits payments across explicit operational milestones verified by physical documentation. Tranches should link to specific checkpoints: component intake clearance, First Article Inspection approval, final assembly pass, and physical arrival at destination. Tying cash releases to verified milestones maintains leverage until every unit meets functional and aesthetic criteria.

Yield Based Tranche Release Mechanics
Yield calculations form the practical math behind final payment releases. In micro batch runs, initial yields fluctuate far more than on mature mass-production lines. A setup phase that scraps twenty circuit boards out of a ten-thousand-unit build produces a minor 0.2 percent scrap rate.
That exact same twenty-board loss on a two-hundred-unit run represents a ten percent scrap rate, wiping out project margins. The settlement framework must define acceptable yield bands and establish tiered payouts tied to verified final output.
Scrap credits require strict documentation. The contract must mandate that final invoice totals automatically adjust for unpassable or scrapped units through predefined deductions. If a contract covers one thousand units at twenty dollars per unit, and the factory delivers nine hundred twenty good units alongside eighty scrapped ones, the final payment must deduct both the piece price of the missing units and the material value of buyer-furnished components destroyed during assembly.
Final tranche payments held until thirty days post-delivery ensure leverage for hidden transit defects or component micro-fractures missed during factory gate checks.
The payment schedule should include a retainage fee ~ typically ten to fifteen percent of contract value ~ held for thirty to sixty days after goods arrive at the buyer’s warehouse. This holdback gives the buyer time to inspect incoming units, unbox shipments, run extended burn-in tests, and verify that substandard packaging didn’t cause hidden damage during transit.
The final payment release checklist governs commercial settlement at the conclusion of a production run:
- Incoming Inspection Reconciliation requires sign-off from the buyer’s warehouse receiving team, confirming total unit counts and outer package condition.
- Functional Sample Audit mandates testing a randomized three percent sample from the shipment under full operating load for seventy-two hours.
- Scrap Log Validation requires auditing factory scrap certificates to account for every damaged or discarded raw component supplied for the run.
- Tooling Cage Verification calls for photographic proof that custom jigs, SMT stencils, and test fixtures are secured in designated factory storage.
- Customs Duty Documentation verifies that export declarations, origin certificates, and shipping manifests match invoice values and tariff entries.

Absorbing Scrap and Rework Costs
Rework during micro batch runs introduces hidden costs that frequently spark commercial disputes. When a batch turns up high defect rates, the factory spends hours desoldering components, re-flashing microcontrollers, or replacing damaged housings. Factories often try to bill those extra labor hours back to the buyer, claiming design complexity caused the defects.
Contract terms must state explicitly that all labor, material, and facility costs associated with non-conformance rework stay strictly with the factory.
Air freight eats margins fast. When rework delays threaten delivery schedules, factories often try to ship via slow ocean freight to protect their own logistics costs. The contract needs to specify that if factory rework delays a shipment by more than five calendar days, the supplier must upgrade transport to expedited air freight at its own expense.
This prevents the factory’s quality failures from pushing delivery slippage onto the buyer’s customers.
| Financial Metric | Agreed Contract Baseline | Actual Line Performance | Net Commercial Settlement |
|---|---|---|---|
| Ordered Volume | 1,000 units @ $45.00/unit | 920 units passed final inspection | $41,400.00 base product credit |
| NRE / Setup Fee | $5,000.00 flat setup rate | Setup completed after 2 line restarts | $5,000.00 (no surcharge permitted) |
| Scrap Allowance | 20 units max absorbed by buyer | 80 units scrapped on SMT line | 60 excess scrap units charged to factory |
| Buyer Component Value | $18.00 per unit provided material | 60 excess scrap units destroyed | -$1,080.00 component loss offset |
| Schedule Slippage | On-time delivery required | 7-day delay due to rework | -$1,400.00 liquidated damages (2%/week) |
| Final Net Invoice | $50,000.00 original total value | Adjusted final delivered output | $43,920.00 final settlement payout |
A negotiated scrap absorption ceiling of 3 percent across all runs ensures that any scrap costs exceeding this threshold are deducted directly from setup and labor settlement balances, subtracting the raw component cost of destroyed units from the final payment. This mechanism keeps suppliers from running uncalibrated lines at the buyer’s expense.
Liquidated damages provisions must be structured carefully to hold up under governing laws like PRC Contract Law or English Commercial Law. Unenforceable penalty clauses simply demand arbitrary fines for delays. Legitimate liquidated damages clauses set out reasonable, pre-calculated estimates of actual commercial loss ~ such as retail late fees, canceled customer orders, or extended warehouse storage.
A standard enforceable approach charges 0.5 percent of total batch value per day of delay, capped at a maximum of fifteen percent of total contract value.
Commercial contracts must also specify the exact currency, exchange rate benchmarks, and banking channels used for settlement. Fluctuations between the US Dollar and local manufacturing currencies (such as the Chinese Yuan RMB) can erode margins quickly during extended builds. The agreement should tie exchange rates to a published central bank reference rate on the date the purchase order is signed, or set a neutral fluctuation band (e.g., plus or minus three percent) within which piece prices stay fixed.
Beyond that band, pricing adjusts based on transparent published benchmarks.
Final invoice settlement closes upon physical receipt of the audited scrap logs and signed factory clearance certificates.